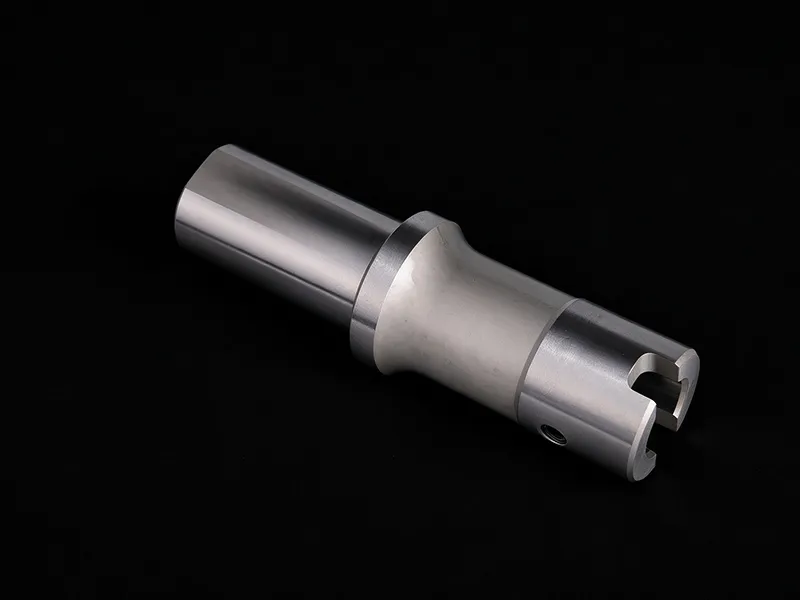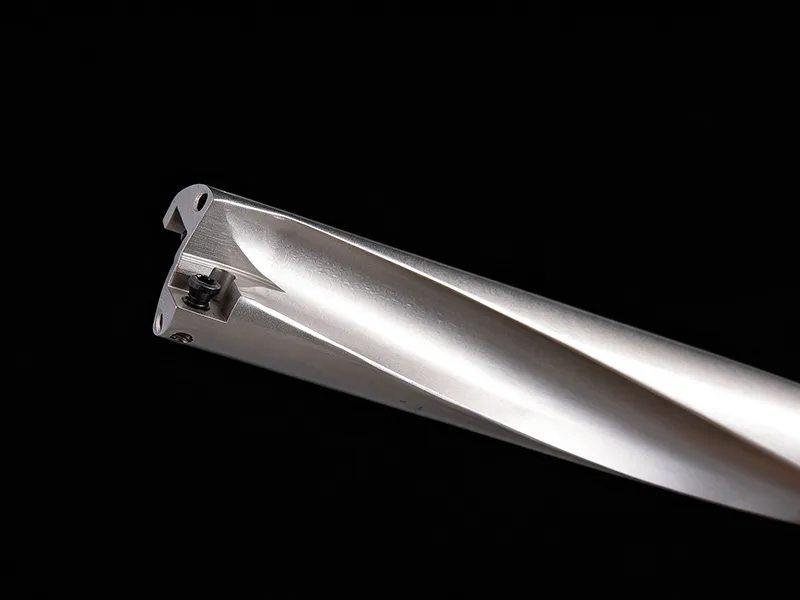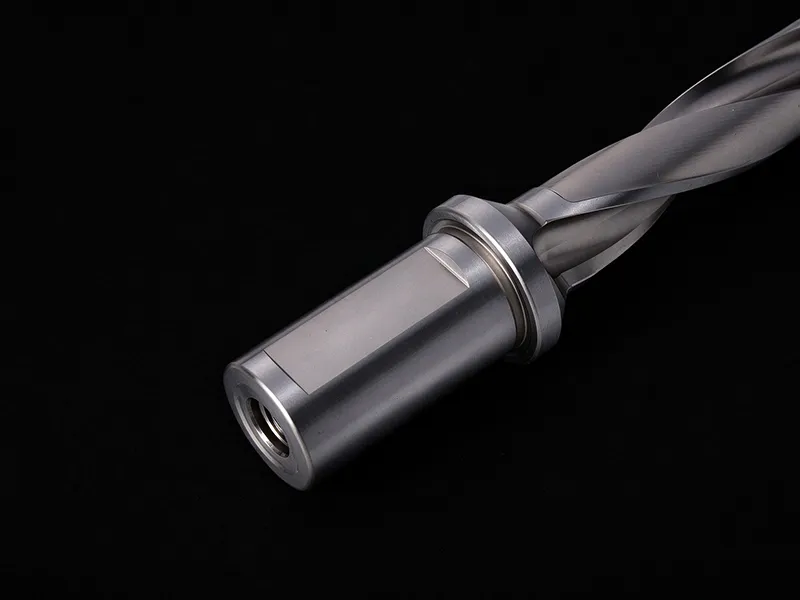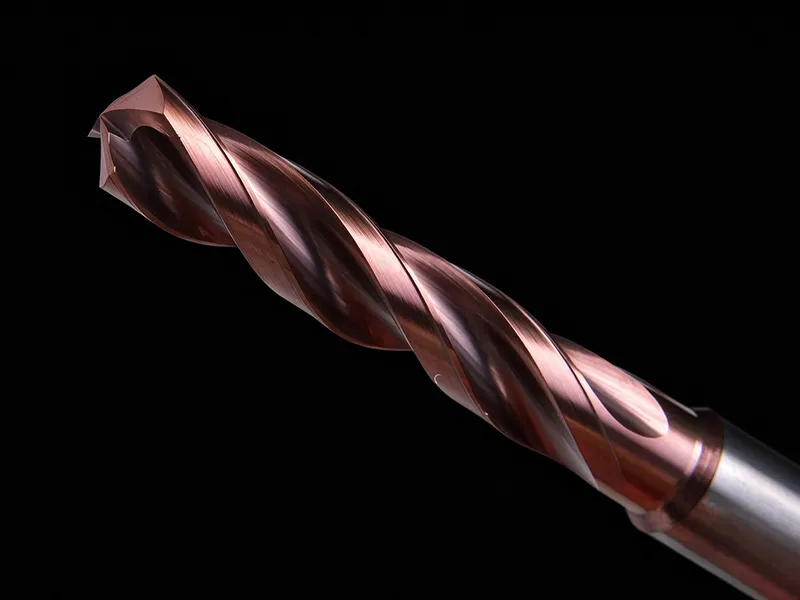
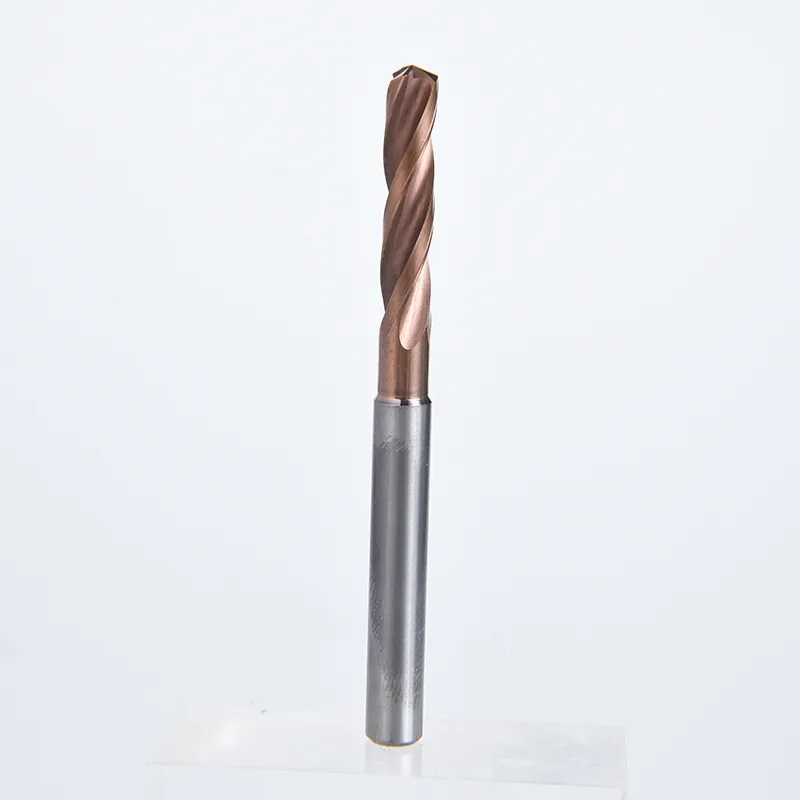
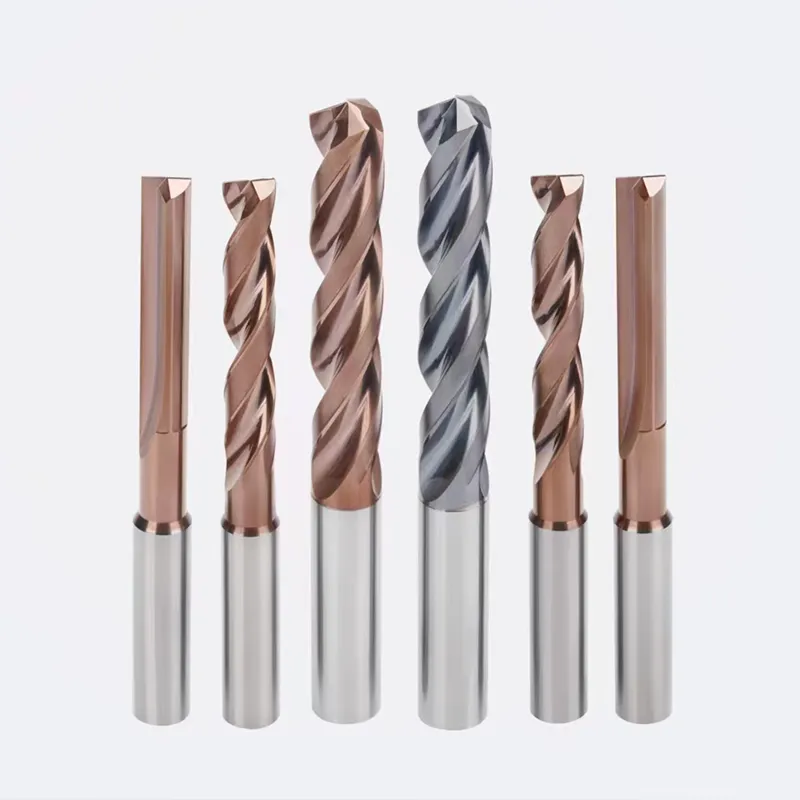
5D 8D Solid Carbide Three Flute Micro Drill Bits
Compare RONGKE 5D 8D Solid Carbide Three Flute Micro Drill Bits for holes beyond the reach of the short DS303C series. This China supplier offers DS305C and DS308C catalogue sizes from Ø5.0 to 12.0 mm. Send the hole drawing for model selection and wholesale pricing based on the required reach.
RONGKE, a drilling-tool manufacturer in China, offers 5D 8D Solid Carbide Three Flute Micro Drill Bits in two length families. The 5D DS305C line covers moderate reach; the 8D DS308C line provides additional drilling depth. Buyers can compare the same cutting diameter across both series before requesting a factory quotation.
A longer tool does not improve a shallow-hole job by itself. The additional length is useful when the hole or access requirement demands it, and places more emphasis on holder accuracy, entry conditions and chip removal.
What Are the 5D and 8D Versions
Both are solid-carbide, three-flute drills with integral cutting edges. Their principal difference is usable depth and associated flute and overall length. At Ø10.6 mm, the catalogue lists Ld 55 mm for DS305C and Ld 90 mm for DS308C; both examples use a Ø12 mm shank.
Advantages of the Two Length Options
5D for the required reach without excess length. Use the intermediate series where the compact 3D version is too short but 8D reach is unnecessary.
8D for deeper features. The longer series extends access while retaining the DS family’s three-edge construction. Its added reach requires a suitable machine setup.
A consistent ordering basis. Both series list m7 cutting diameters and h6 shanks, with matching P/K/M/A workpiece codes. Series and depth must still be stated separately on the order.
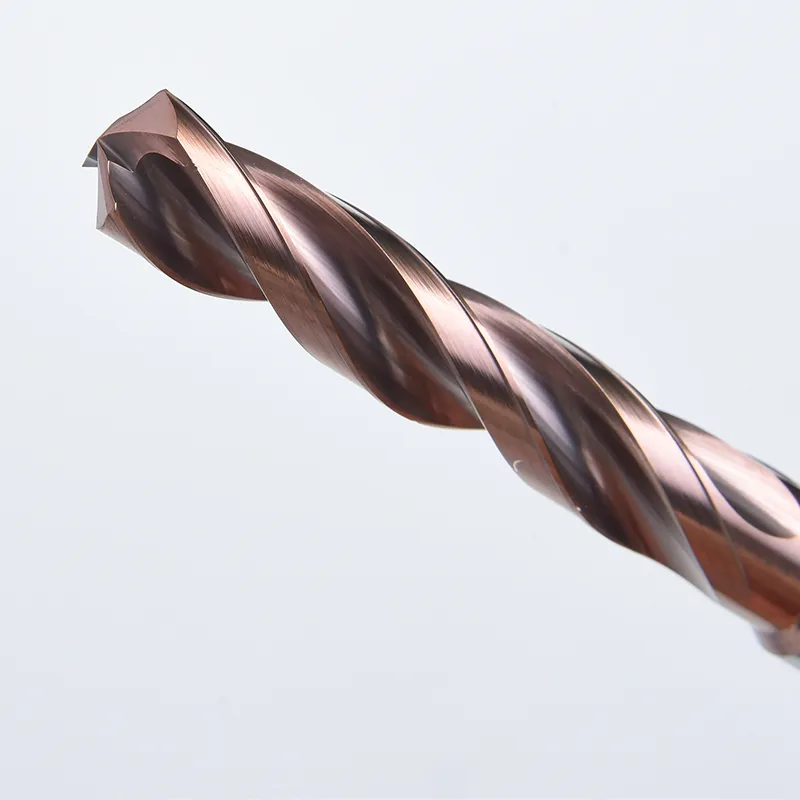
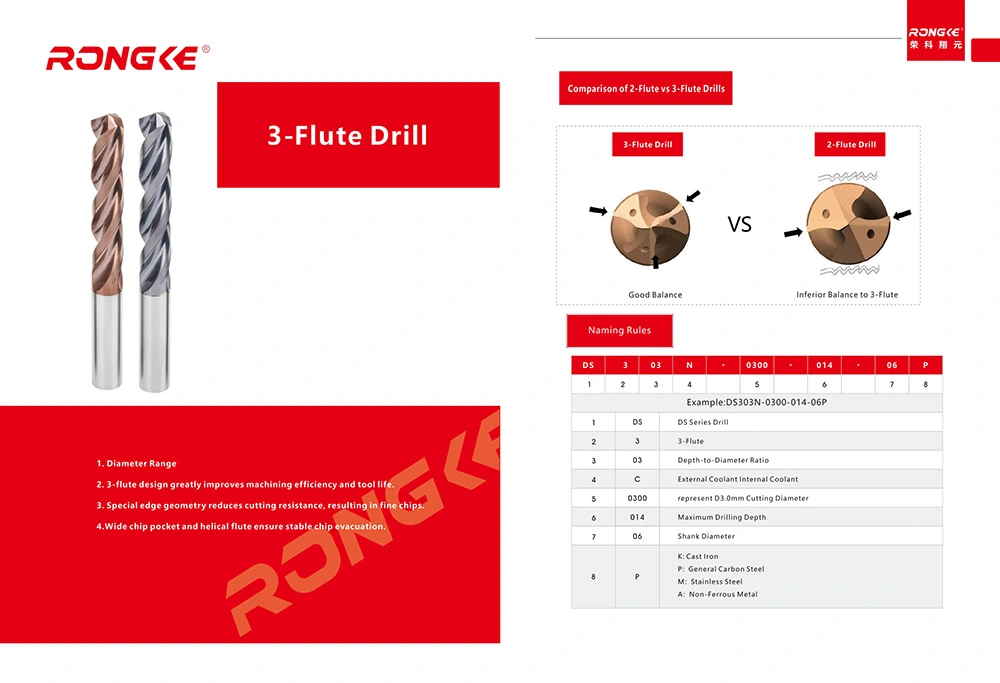
Geometry for chip formation and transport. The catalogue combines special cutting edges with wide chip pockets and helical flutes. This is a design feature, not a fixed percentage improvement in speed or tool life.
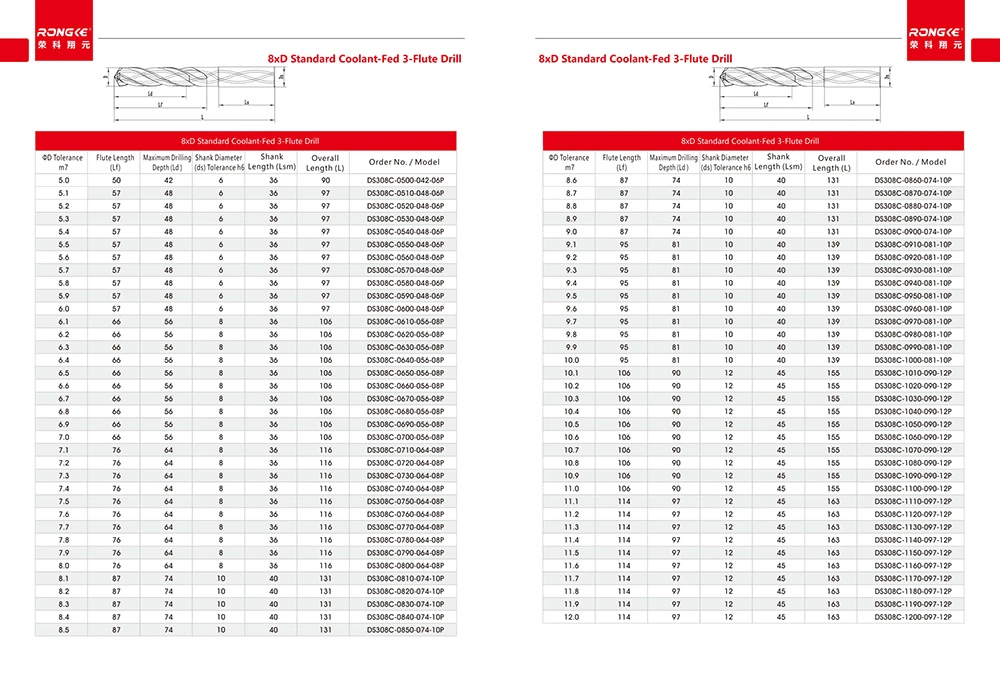
Specifications
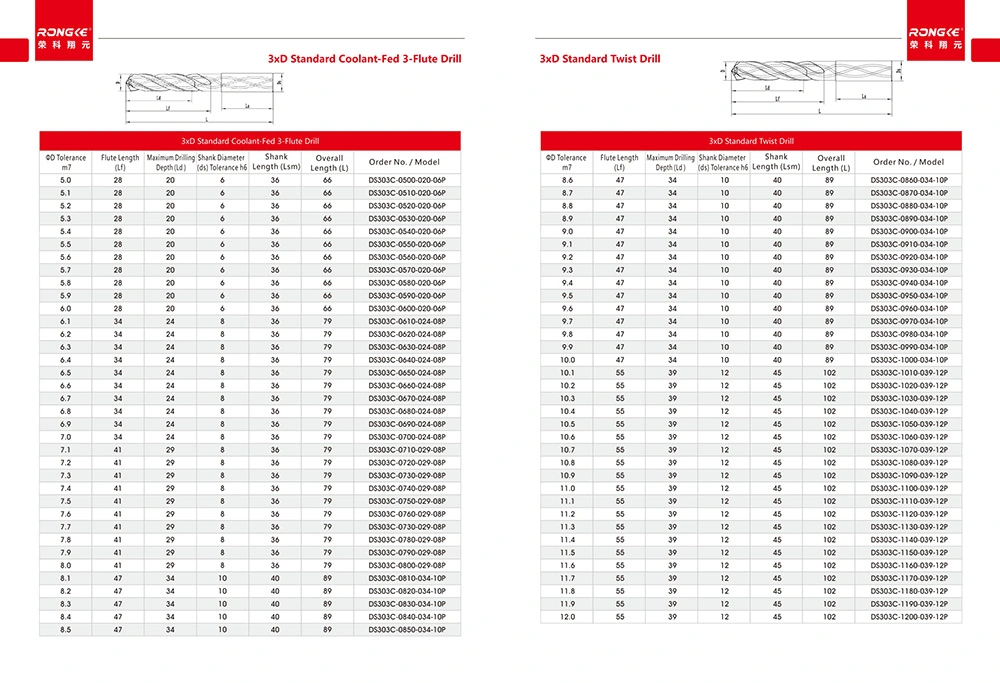
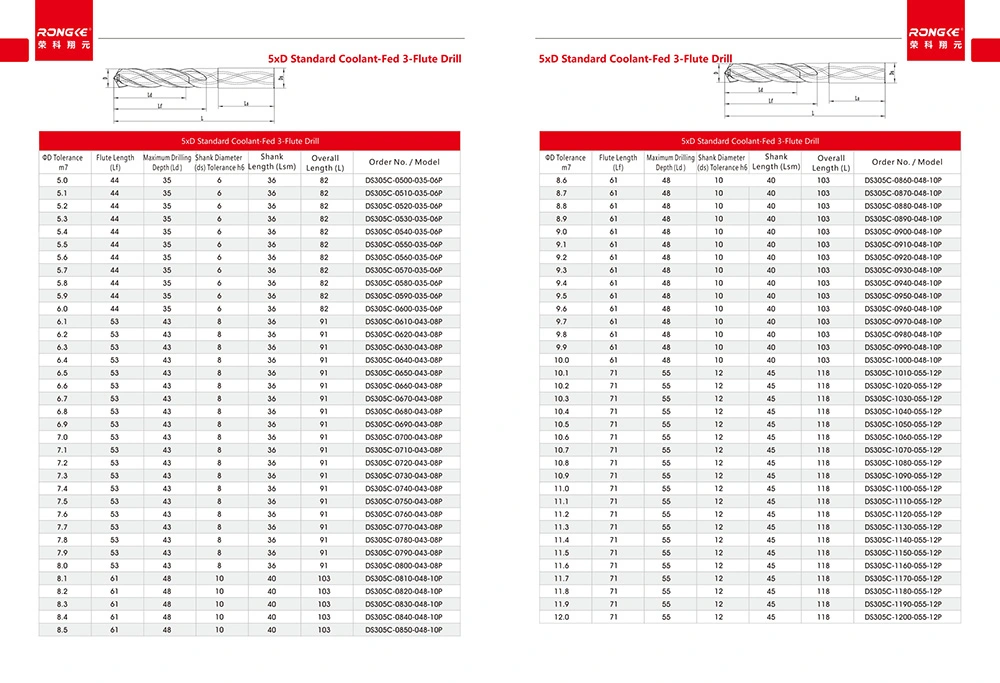
Dimensions in mm. Cutting diameters run from Ø5.0 to 12.0 in 0.1 mm increments. The grouped table keeps drilling depth separate from the flute length.
|
Series |
Cutting Ø |
Max. Ld |
Flute Lf |
Shank Ø |
Overall L |
|
5D |
5.0–6.0 |
35 |
44 |
6 |
82 |
|
5D |
6.1–8.0 |
43 |
53 |
8 |
91 |
|
5D |
8.1–10.0 |
48 |
61 |
10 |
103 |
|
5D |
10.1–12.0 |
55 |
71 |
12 |
118 |
|
8D |
5.0 |
42 |
50 |
6 |
90 |
|
8D |
5.1–6.0 |
48 |
57 |
6 |
97 |
|
8D |
6.1–7.0 |
56 |
66 |
8 |
106 |
|
8D |
7.1–8.0 |
64 |
76 |
8 |
116 |
|
8D |
8.1–9.0 |
74 |
87 |
10 |
131 |
|
8D |
9.1–10.0 |
81 |
95 |
10 |
139 |
|
8D |
10.1–11.0 |
90 |
106 |
12 |
155 |
|
8D |
11.1–12.0 |
97 |
114 |
12 |
163 |
Source: RONGKE MAIN CATALOG, PDF pages 66–67 of 69. Cutting diameter m7; shank h6. Both tables are labelled coolant-fed; confirm the supply connection and required flow for the selected tool. No replaceable insert is used.
Selection Advice
Depth and access. Choose 5D 8D Solid Carbide Three Flute Micro Drill Bits by the required Ld and overall access, not the series name alone. At Ø10.6 mm: DS305C-1060-055-12P has L 118 mm; DS308C-1060-090-12P has L 155 mm.
Entry and support. Review angled faces, cross holes and interrupted entry before setting the drilling cycle. A pilot or other preparation is application-specific, not an automatic requirement for every 8D job.
Machine and coolant. Assess clamping length, tool run-out and available coolant delivery together. Specify whether the hole is blind or through; chips have a longer exit path in the deeper series.
Material and acceptance. Confirm the material grade, hardness and required hole finish before choosing P, K, M or A. Validate the proposed process on the actual component when the tolerance is critical.
Inspection Process
For a long-reach order, agree the inspection scope before production. The following sequence identifies useful acceptance checks; inspection reports, test cutting and numerical limits must be confirmed with RONGKE for the order.
1. Verify the selected series. Compare diameter, Ld, flute length, overall length and shank with DS305C or DS308C dimensions. This prevents a shorter tool being accepted for a deeper-hole requirement.
2. Review cutting geometry and assembly accuracy. Check the cutting edges and shank condition, and agree how tool run-out will be evaluated. Holder and spindle effects need separate attention during setup.
3. Assess the application where needed. For an agreed cutting trial, record the workpiece, holder, coolant and cutting data alongside hole measurements. One successful trial does not guarantee identical results in a different setup.
FAQ
Is 8D automatically the better option?
No. Additional reach is useful only when needed. If 5D reaches the feature with adequate clearance, its shorter configuration is generally the more rigid choice.
Can I use flute length as the allowed drilling depth?
No. Lf includes flute length beyond the listed maximum drilling depth Ld. Use the model’s Ld and confirm the point and breakthrough requirements on the drawing.
Must every 8D hole be pilot-drilled?
There is no universal cycle for all entries and materials. Share the entry surface, depth and machine setup so the starting sequence can be reviewed.
Do all 5D and 8D sizes need the same coolant pressure?
No single pressure is specified in these catalogue tables. Tell the supplier the machine’s coolant capability and hole geometry before committing to a long-reach application.
Can I assume the same cutting parameters for both series?
No. Greater depth changes chip travel and setup sensitivity. Use the recommended data for the actual model, then evaluate chip formation and hole quality during the trial.
How can a distributor avoid mixing the two lengths?
Order 5D 8D Solid Carbide Three Flute Micro Drill Bits by complete model and quantity, not diameter alone. Separate DS305C and DS308C on the purchase list, especially where the shank and cutting diameter are identical.
Related Category
Send Inquiry
Contact Info
-
Address
No. 399 Haohai Road, Binhai New Area, Economic Development Zone, Fenghua District, Ningbo City, Zhejiang Province, P.R.China
-
Tel
-
Email
Request a quotation from RONGKE for standard U drills, modular deep hole drills and customized CNC cutting tools. Share your machining requirements, tool dimensions and order quantity for professional product recommendations.
News Recommendations