Factory Direct Replaceable Head Drills
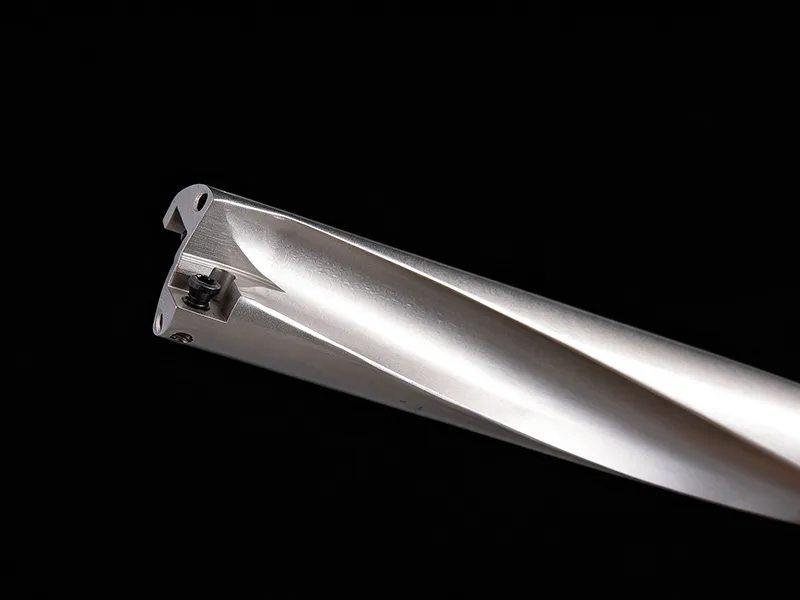
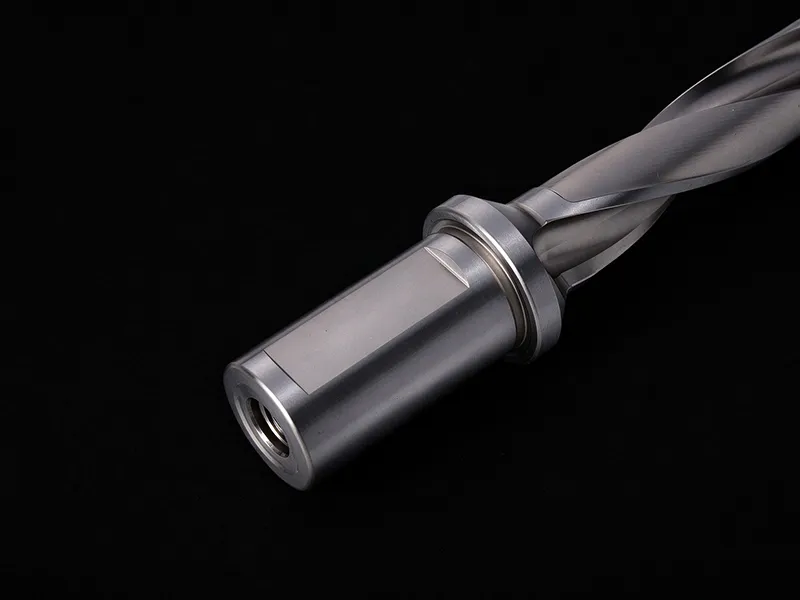
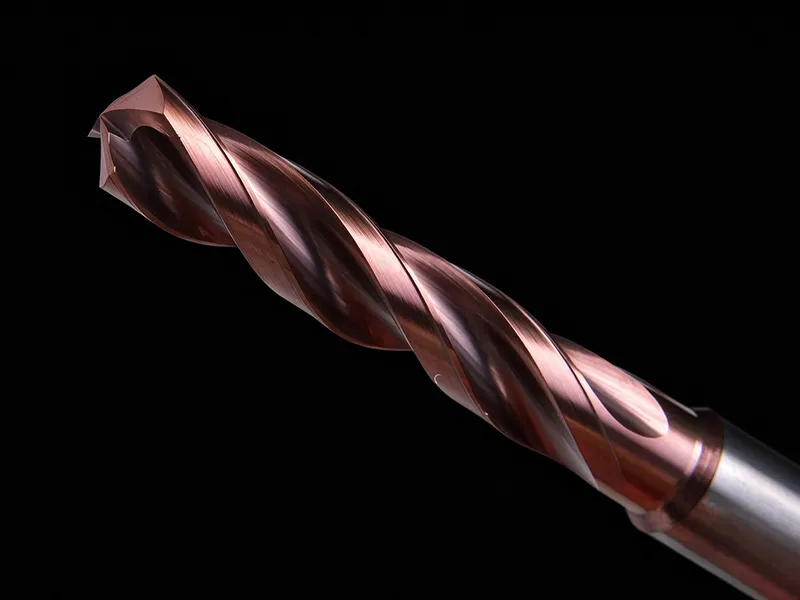
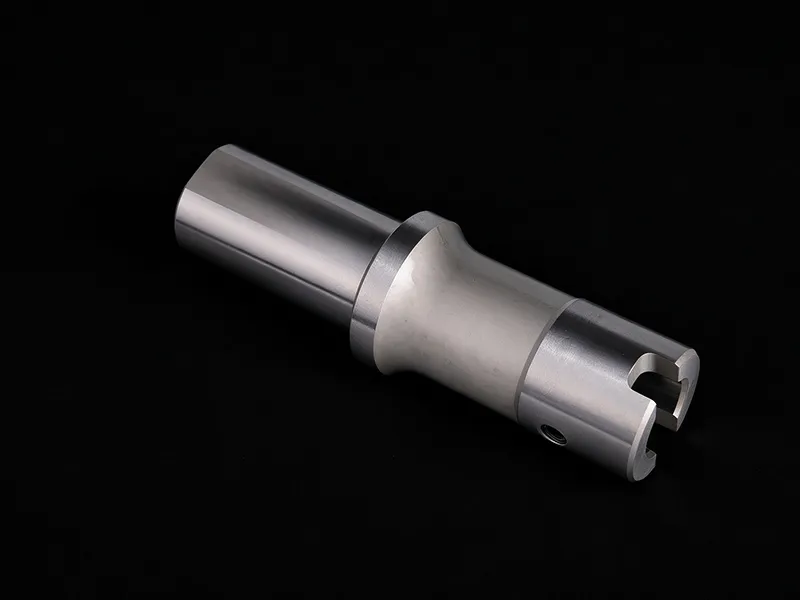
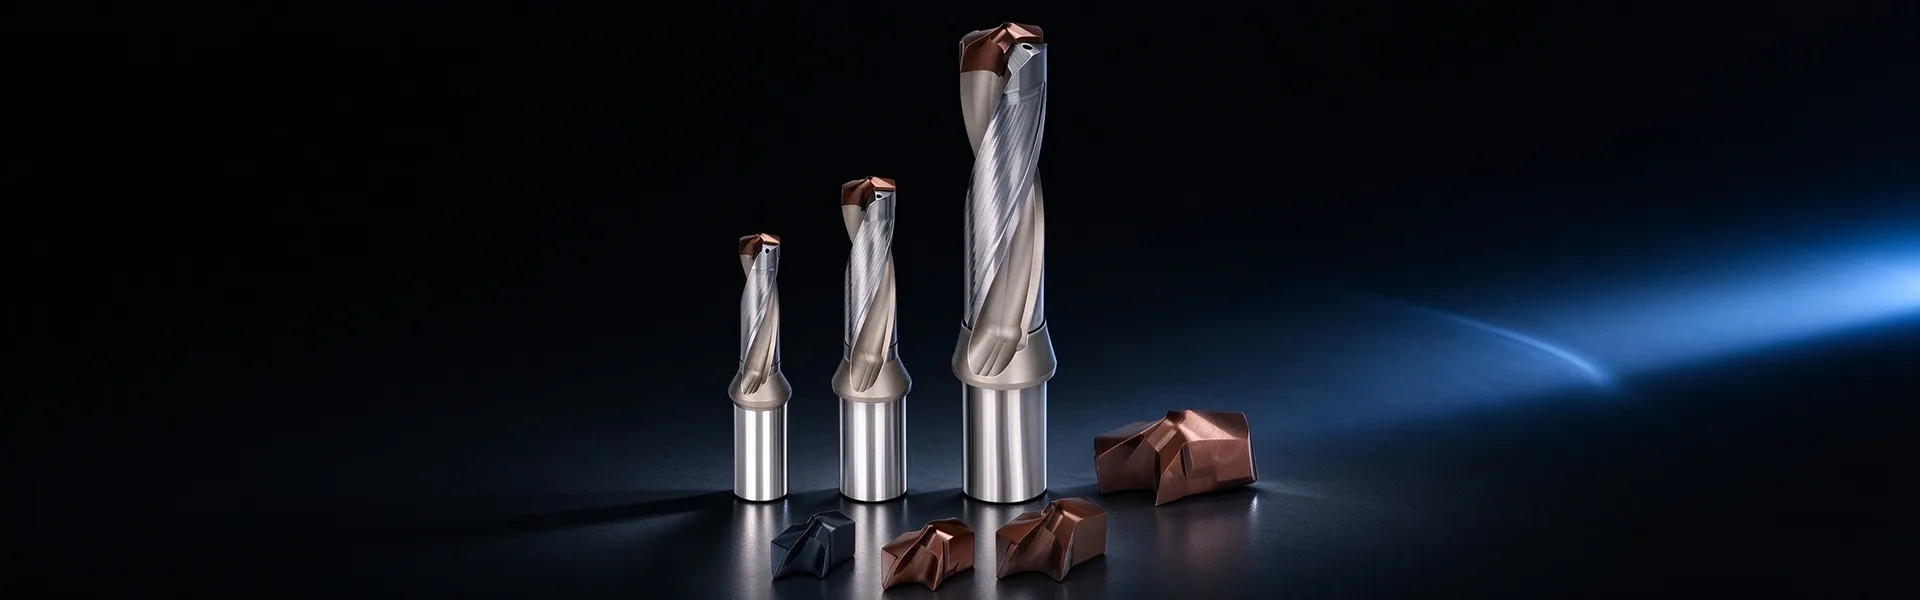
For machine shops and production lines that drill thousands of holes per shift, tooling cost per hole is one of the most important key performance indicators on the shop floor. A worn drill tip usually means stopping the spindle, removing the tool, sending it out for resharpening, and re-measuring tool offsets. Replaceable Head Drills change that workflow completely. RONGKE has engineered a comprehensive series of replaceable head drills that keep a reusable alloy steel body in the toolholder while only the carbide head is replaced.
Applications Across Industries
- Automotive manufacturing: Drilling engine blocks, brake calipers, steering knuckles, and transmission housings. The 3D and 5D bodies cover most flange and housing drilling operations, while the quick head change supports high-volume part changeover.
- Aerospace components: Drilling stainless steel and titanium structural parts. The internal coolant design and AlCrN coating help control heat in difficult materials. The 8D and 12D options are suitable for deep spar and rib holes.
- Energy and power generation: Drilling tube sheets, flanges, and heat exchanger plates. Replaceable head drills reduce tool inventory for large-diameter holes and improve repeatability in automated drilling cells.
- Mold and die manufacturing: Pre-drilling deep water lines and ejector pin holes in tool steel. The stable length reference and standard shank interfaces make these drills a practical choice for high-precision mold work.
- General machining and job shops: Mixed-material shops benefit from body reuse across different jobs. A single body can accept different coating heads for steel, stainless steel, or aluminum, reducing the number of complete tools in inventory.
Selecting the Right RONGKE Cutting Head for Different Materials
Choosing the correct head geometry and coating has a direct impact on tool life and hole quality. RONGKE offers three standard point angles. The 140° self-centering point is the best general-purpose choice for steels and cast iron because it reduces cutting forces and improves hole position. The 130° point is designed for stainless steel and high-temperature alloys where heat control is critical. The 118° point is a traditional geometry often preferred in aluminum and non-ferrous materials to reduce burr formation. Coatings should match the workpiece: TiAlN for steel and cast iron, AlCrN for stainless steel and difficult alloys, and DLC for aluminum and other non-ferrous metals where built-up edge must be avoided.
The chip breaker also matters. The standard chip breaker works well for most drilling operations with feed rates from 0.08 to 0.15 mm/rev. The fine-finish chip breaker is designed for low-feed finishing passes where surface finish in the hole is important. The high-feed chip breaker can handle feed rates up to 0.25 mm/rev in aluminum and low carbon steel, increasing productivity in non-critical holes. RONGKE application engineers can recommend the best combination based on your specific part material, machine capability, and tolerance requirements.
Maintenance and Tool Life Optimization
To get the most value from replaceable head drills, shops should monitor wear patterns on the cutting head. A normal wear pattern shows a smooth, even flank wear along both cutting edges. Irregular wear, chipping, or built-up edge usually indicates a problem with cutting speed, feed rate, coolant pressure, or workpiece clamping. When the average flank wear reaches 0.2–0.3 mm, the head should be replaced. Running the drill beyond this point risks damaging the body interface and increases the chance of tool breakage.
Coolant is especially important. RONGKE recommends a minimum coolant pressure of 10 bar for 3D drilling in steel and 20 bar or more for 5D and 8D depths. The twin coolant outlets on each head direct fluid to the cutting edges, helping to break chips and carry them out of the hole. For deep-hole drilling, pecking cycles or pilot-hole preparation may be required. In cast iron, air blast or minimum quantity lubrication is often sufficient, but the cutting speed should be adjusted to prevent abrasive wear on the head.
Frequently Asked Questions
Q: Can I use the same body with different diameter heads?
A: No, each body is matched to a specific diameter range. A RONGKE body designed for a 12.0–13.9 mm head will not properly fit a 10.0–11.9 mm or 14.0–15.9 mm head. The conical interface and radial stop are ground to match the head size. However, within the same diameter range, you can switch between different point angles, coatings, and chip breaker geometries. This gives you flexibility for different workpiece materials without buying complete new tools.
Q: What coolant pressure is required?
A: RONGKE recommends 10–15 bar minimum for 3D drilling in low and medium carbon steel. For 5D and 8D drilling, coolant pressure should be 15–25 bar to ensure proper chip evacuation. In stainless steel, titanium, and high-temperature alloys, use 20–30 bar. If your machine has through-spindle coolant capability, match the pump to the body coolant inlet size. Inadequate pressure leads to chip packing, poor hole finish, and reduced head life. For deep-hole applications with 12D drilling, a pilot hole and pecking cycle may be needed in addition to high coolant pressure.
Q: How many times can a RONGKE replaceable head drill body be reused?
A: The steel body is designed for repeated head changes. In controlled production conditions, a body can typically be reused for 50 to 80 head replacements, depending on the material being drilled and the operator’s care during head changes. The main causes of body damage are over-tightening, debris on the interface, and running a completely worn or broken head. If the body’s conical taper is inspected periodically and proper torque specifications are followed, it will provide long service life. RONGKE includes a go/no-go gauge with each body to help users check interface wear.
Q: What torque should I use when mounting a new head?
A: The recommended tightening torque depends on the diameter range. For 8.0–11.9 mm bodies, use 1.5 Nm. For 12.0–16.9 mm, use 2.0 Nm. For 17.0–25.9 mm, use 2.5 Nm. Always use a calibrated torque wrench and the RONGKE head removal key. Do not use a standard wrench or pliers, as this can damage the head or the interface. After tightening, check the axial stop to make sure the head is fully seated. If the head is not fully seated, cutting forces can cause vibration and poor hole quality.
- View as
Replaceable Spade Drill Inserts
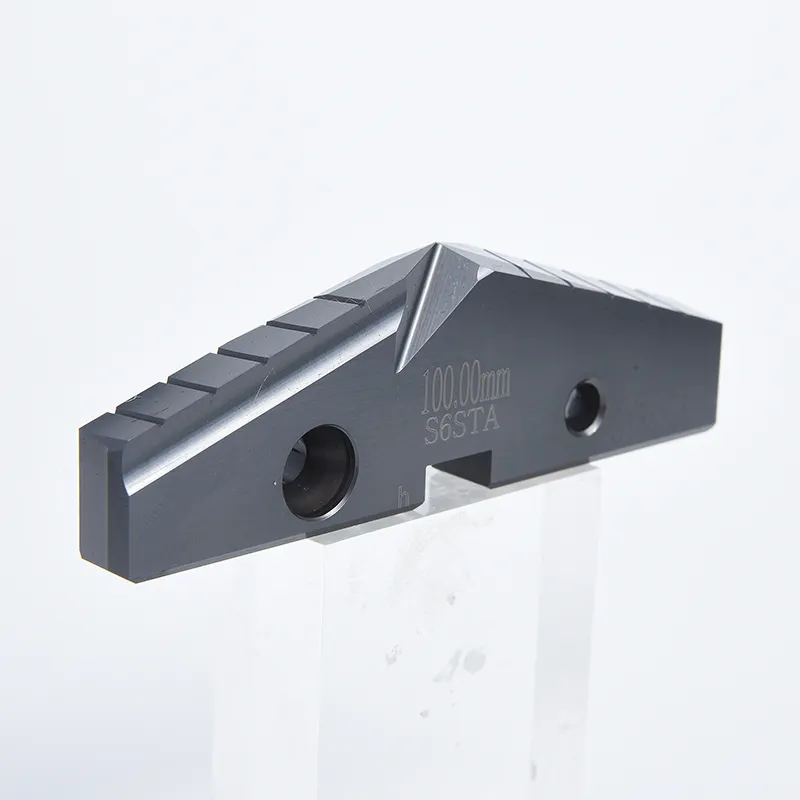
RONGKE replaceable spade drill inserts are available in cobalt high-speed steel, powder high-speed steel and carbide. Select the substrate, chipbreaker and coating to match the workpiece, machine rigidity and hole depth.
Replaceable Blade Deep Hole Spade Drill
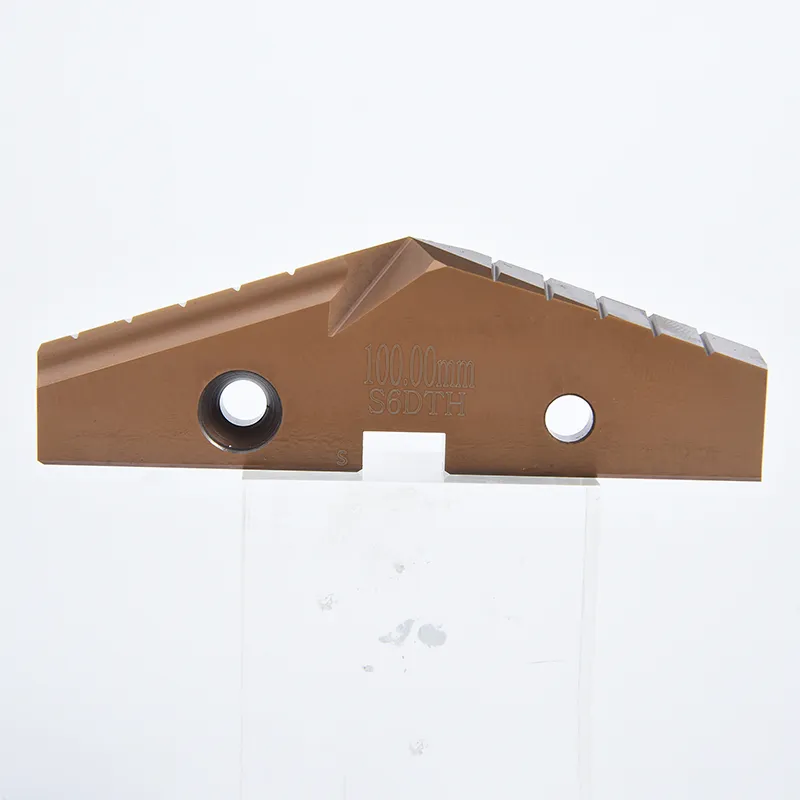
For workshops using different shank connections, RONGKE Replaceable Blade Deep Hole Spade Drill supports selection around the blade group and the machine-side shank connection. Contact us for replacement-part orders. Side-lock and Morse-taper holders serve different machine connections, while S2, S6 and G2 blade options support material selection. Request the matched blade and holder group.
Replaceable Head Saber Tooth Drill Holder
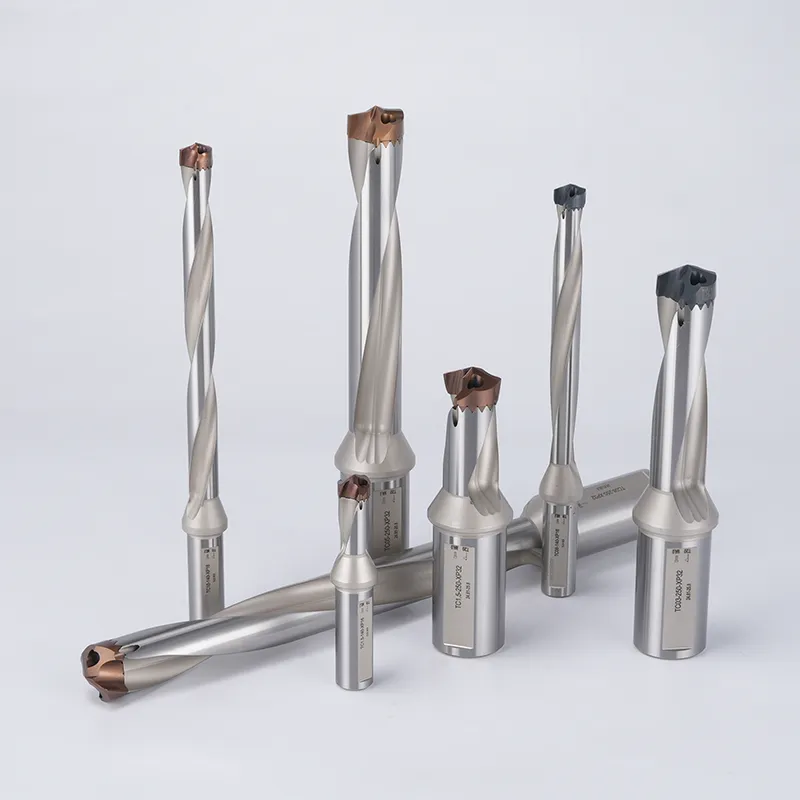
For a body-only order or a complete TC assembly, RONGKE Replaceable head saber tooth drill holder supports selection around the usable reach and seat of the TC body. Contact us for supplier quotations. The catalog spans 1.5D–12D, with diameter availability varying by series. Choose the required effective length and holder seat when ordering a body or complete assembly.
Replaceable Saber Tooth Drill Tips
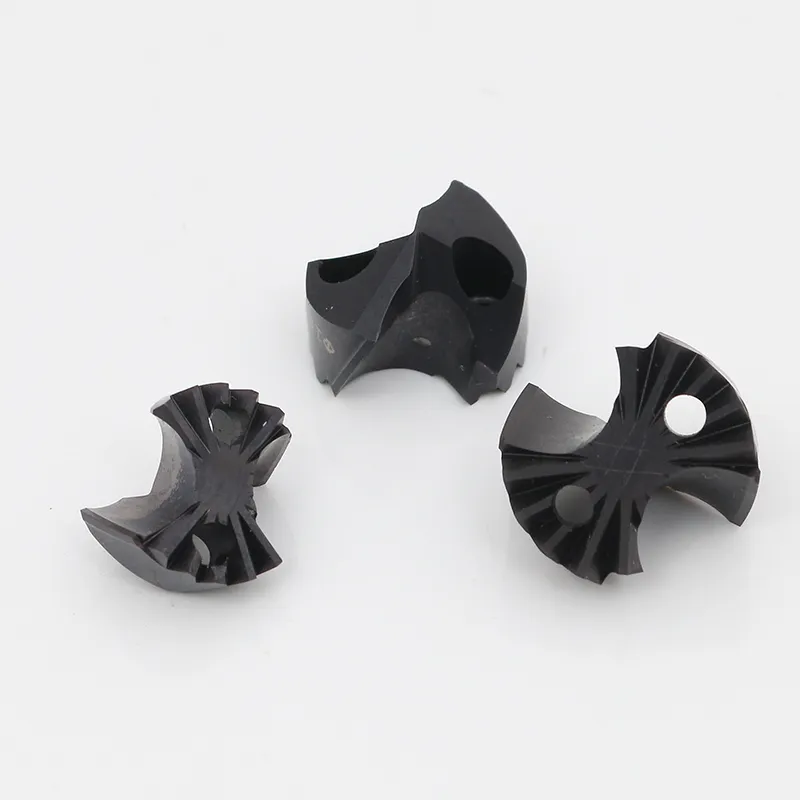
When renewing the cutting end of a TC assembly, RONGKE Replaceable Saber Tooth Drill Tips supports selection around the cutting geometry of the replacement TC tip. Contact us for spare-tip quotations. The Ø12.0–33.5 mm family supports the saber system’s focus on accuracy, efficiency and convenient tip changes. Request replacements by tip geometry and holder seat, rather than body depth.
Replaceable Phoenix Drill Tips
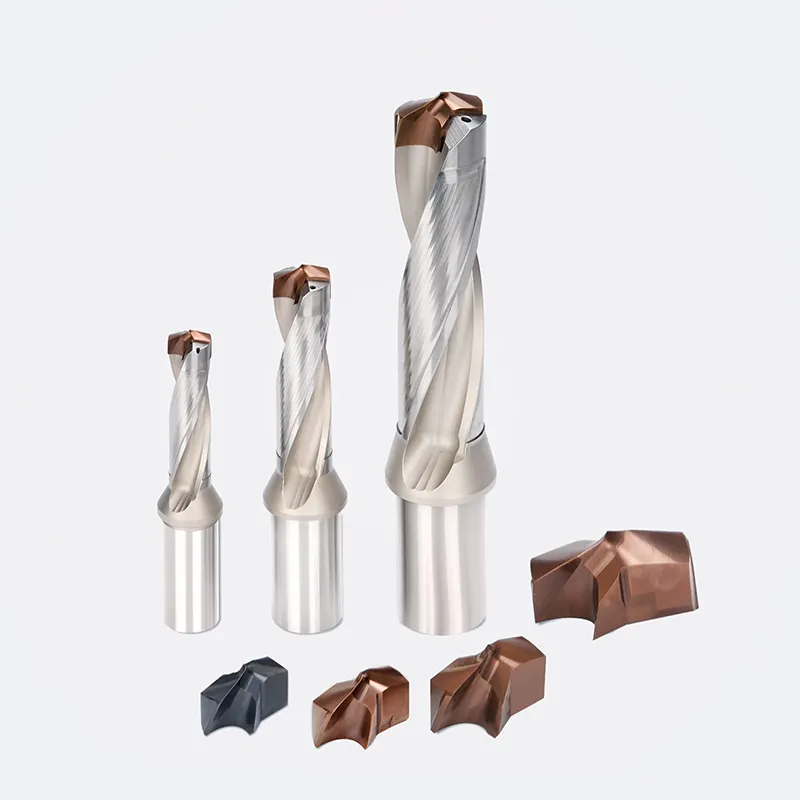
For spare-tip purchasing, RONGKE Replaceable Phoenix Drill Tips supports selection around tip diameter and Phoenix seat compatibility. Contact us for replacement-part orders. Select Ø12.50–52.00 mm tip diameter, PDPA/PDGA/PDMA geometry and the matching seat. Body depth ratios are separate from tip size; include both references when ordering spares.
Replaceable Head Phoenix Drill PD
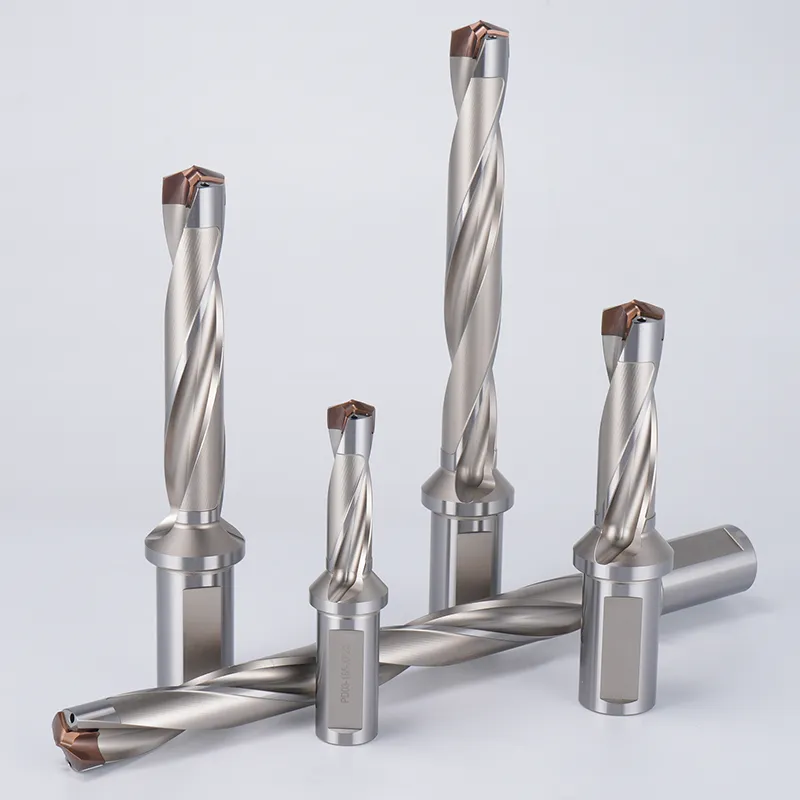
Where the Phoenix configuration requires margins, RONGKE Replaceable Head Phoenix Drill PD supports selection around the PD margin design at the same PT diameter and reach. Contact us for purchase planning. It shares PT specifications and the family’s balance of price, efficiency and accuracy. Order by PD body reference, cutting diameter and required reach.
RONGKE supplies Replaceable Head Drills directly from our factory. Get in touch today for pricing and orders!
News Recommendations