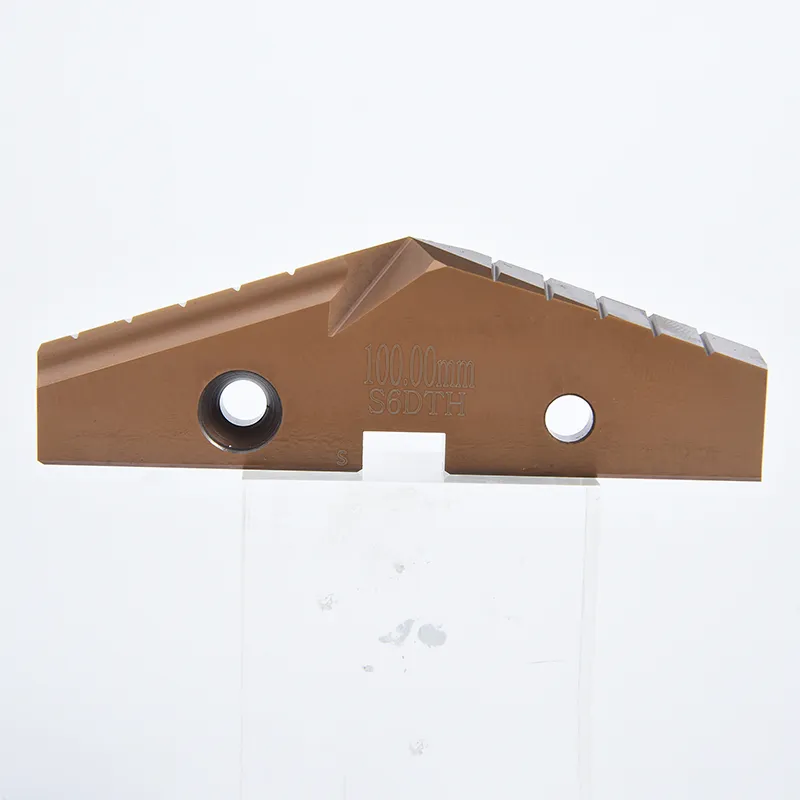
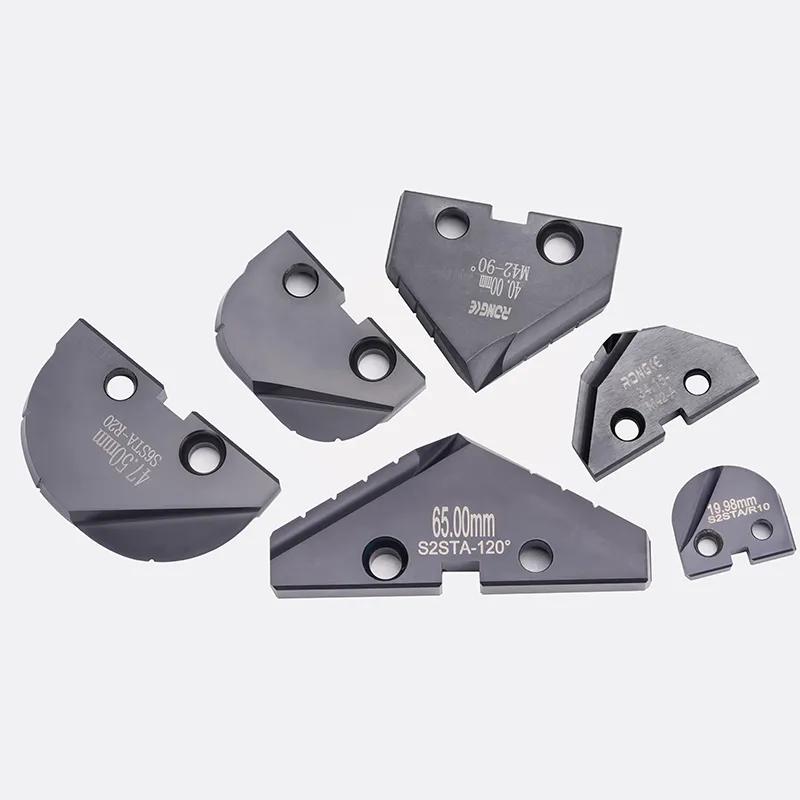
Replaceable Spade Drill Inserts
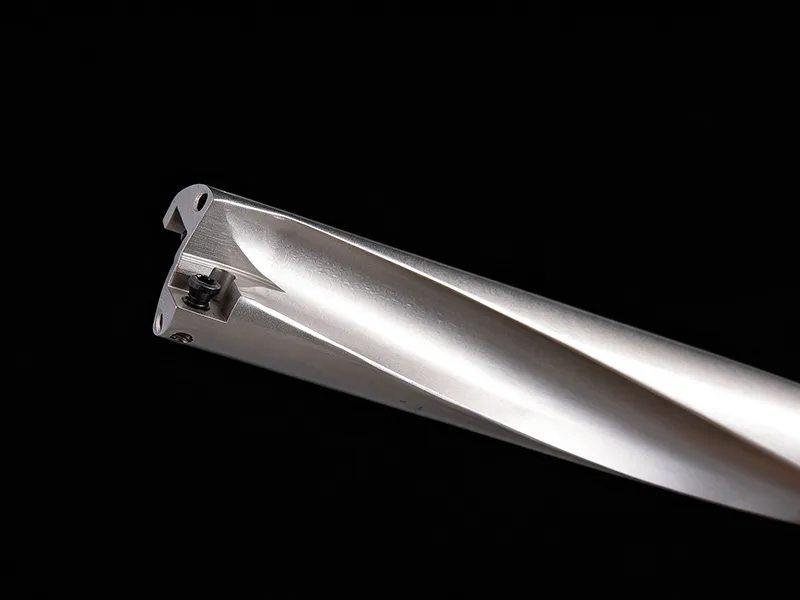
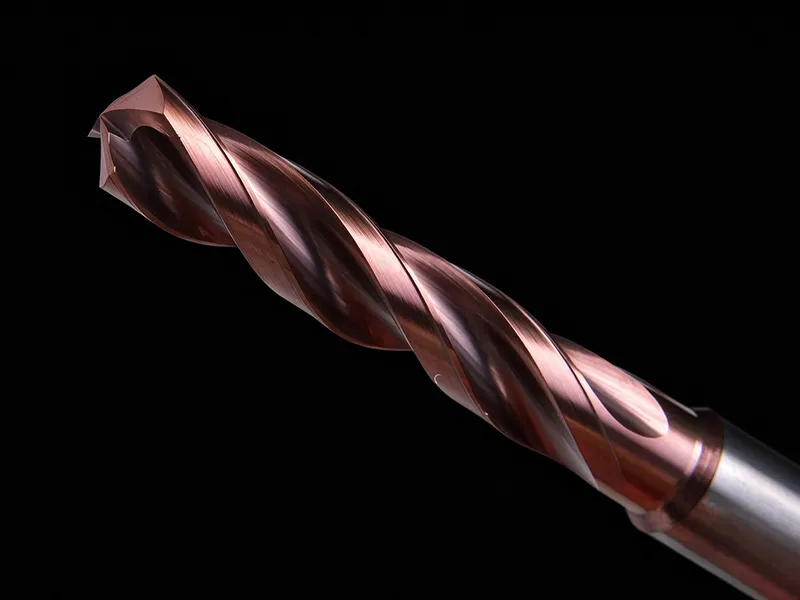
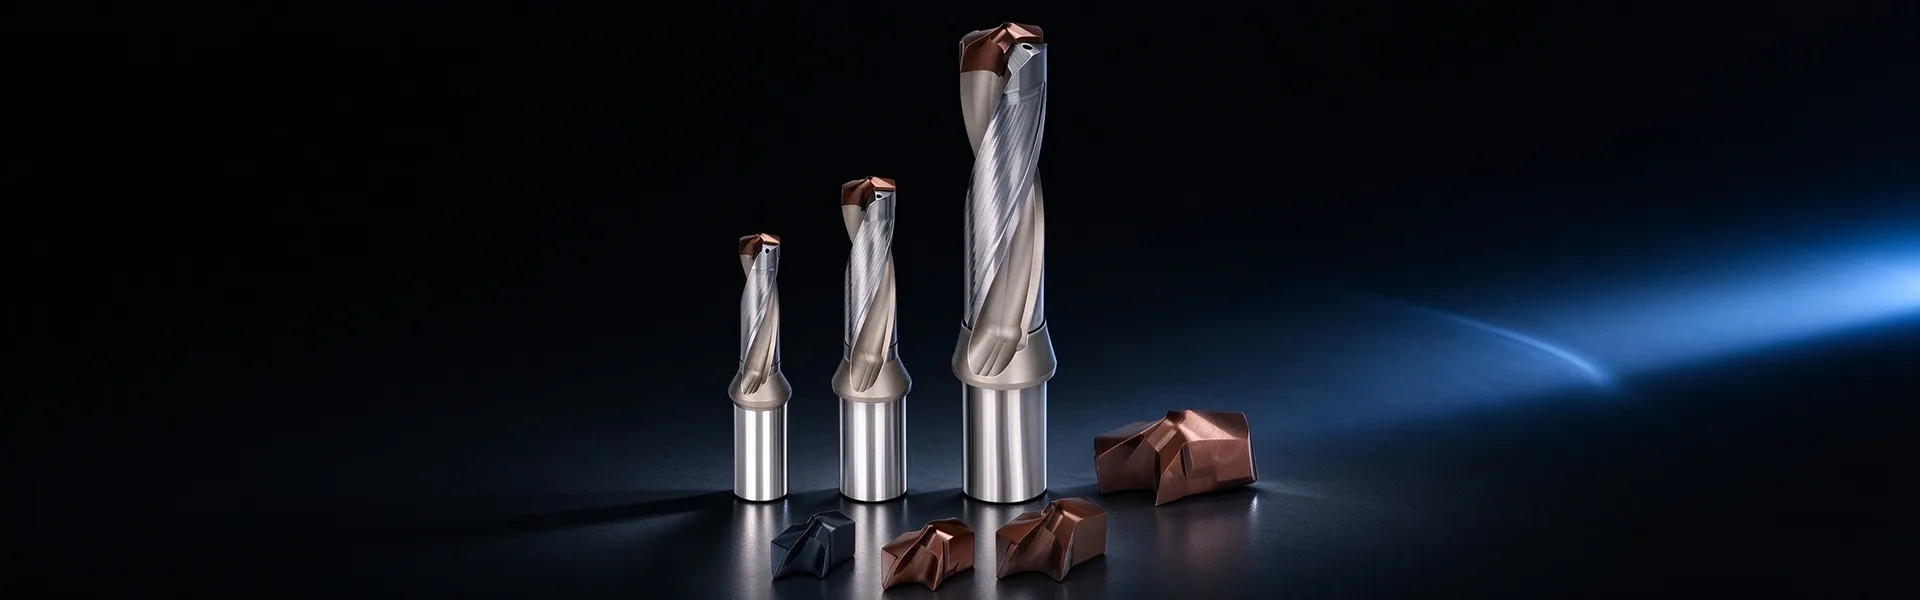
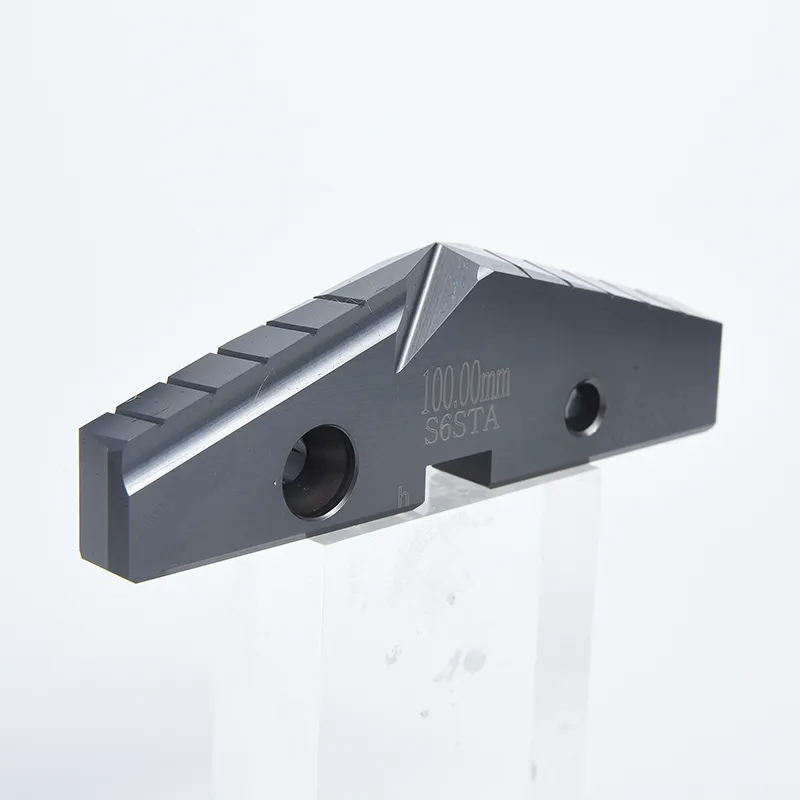
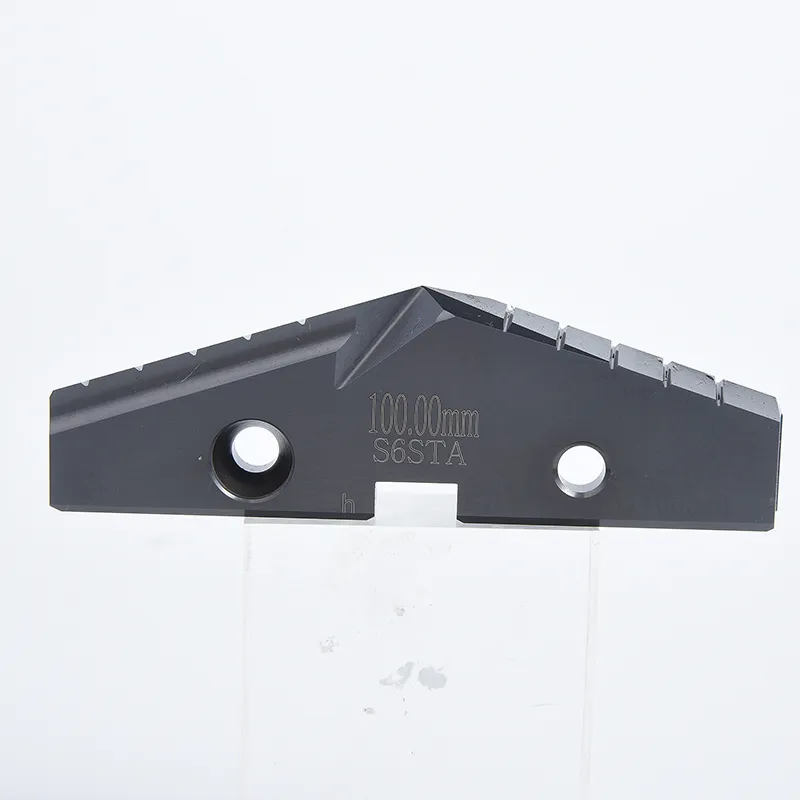
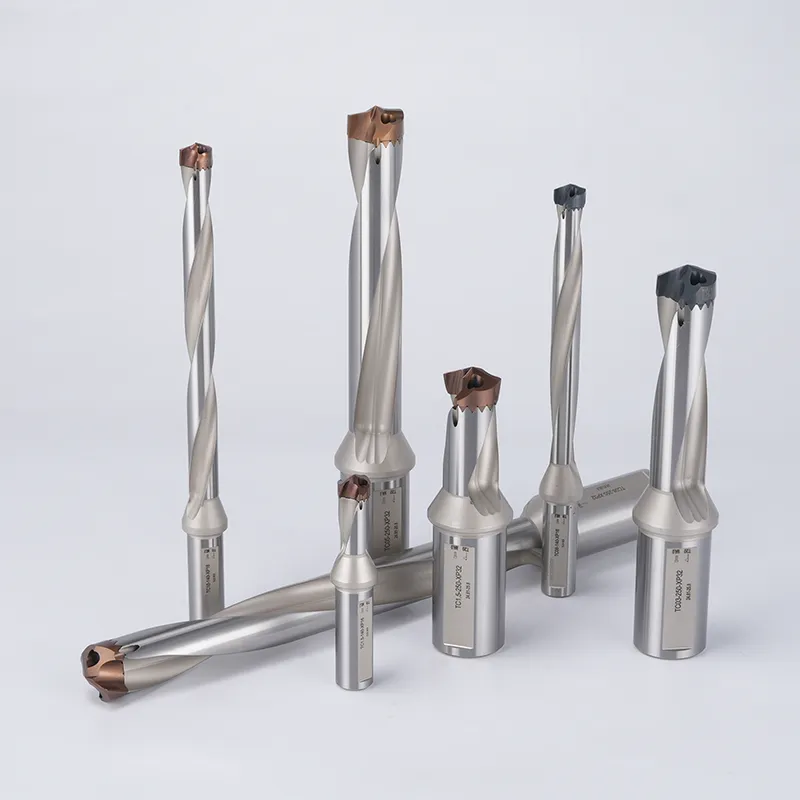
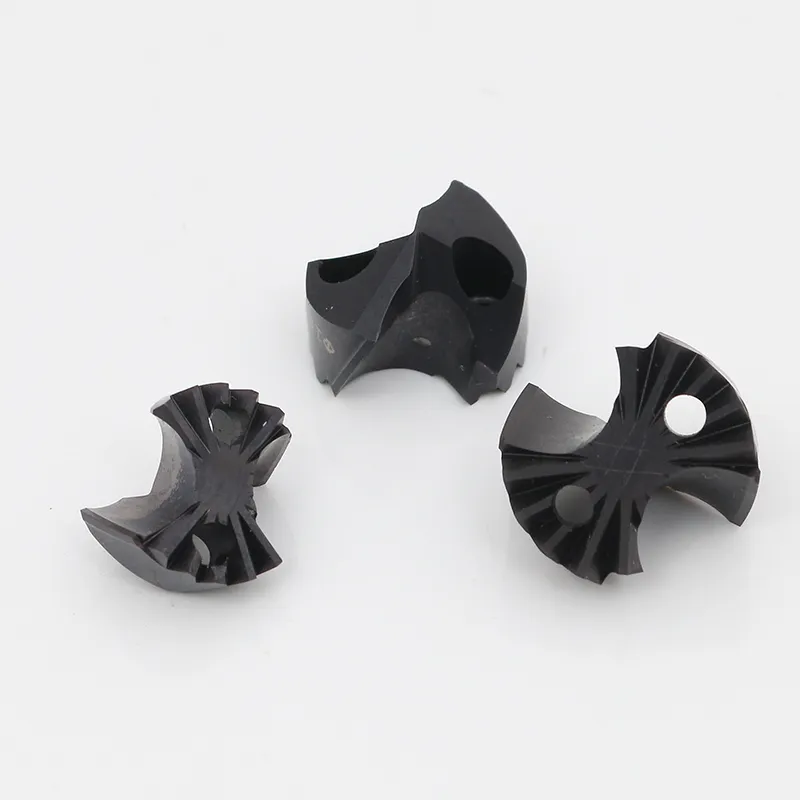
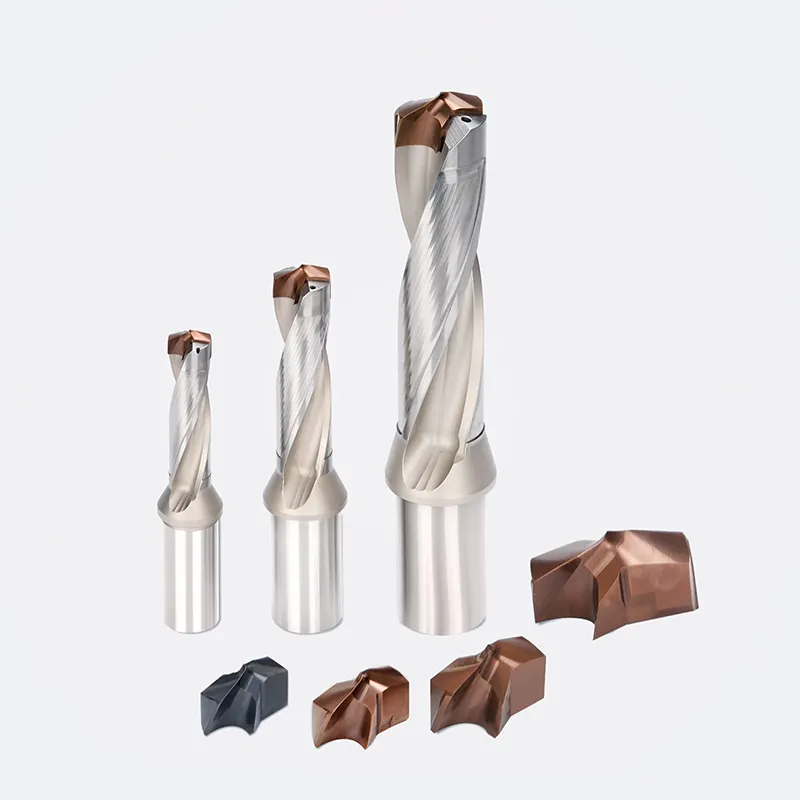
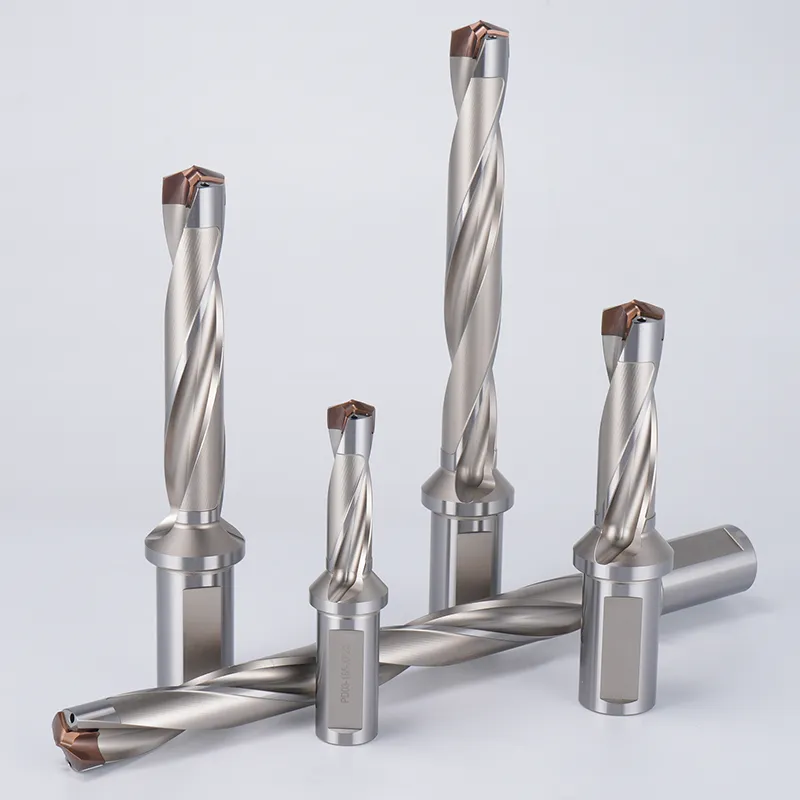
RONGKE replaceable spade drill inserts are available in cobalt high-speed steel, powder high-speed steel and carbide. Select the substrate, chipbreaker and coating to match the workpiece, machine rigidity and hole depth.
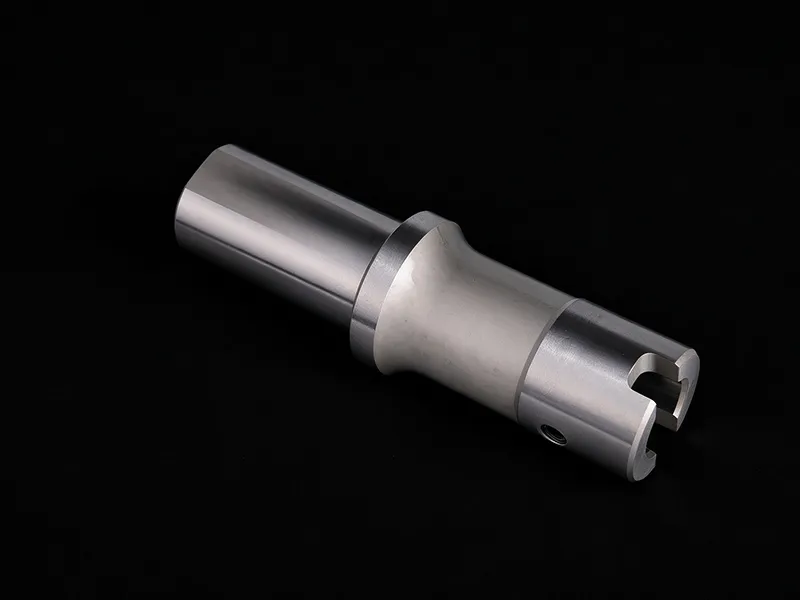
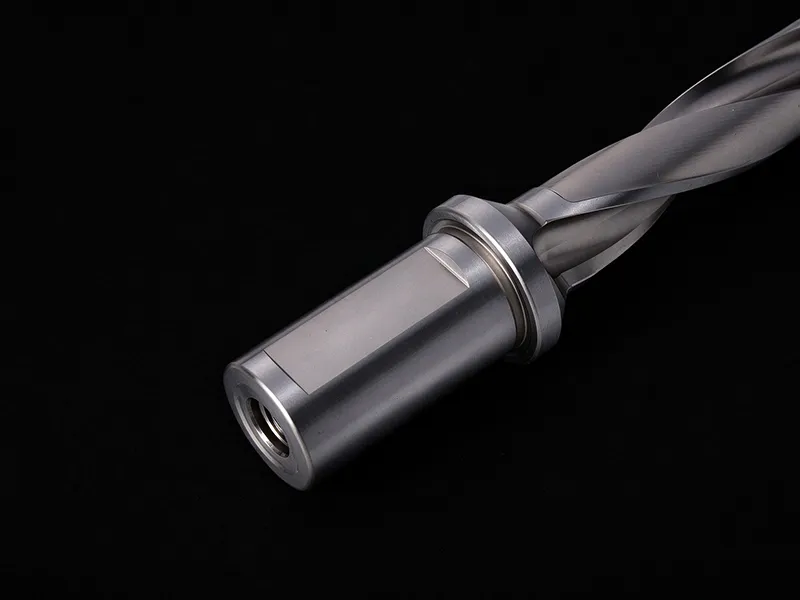
A locating pin positions the flat insert in the drill body seat, and matching screws clamp it in place. Clean the Replaceable spade drill inserts’s seat and match the insert diameter, thickness and point angle before installation.
Product Introduction
|
Code and material |
Selection focus |
Listed variants |
|
S2 - Cobalt high-speed steel |
Higher toughness than carbide; suitable for conventional machines and longer-reach drilling. |
S2STA / S2DTH / S2DTP |
|
S6 - Powder high-speed steel |
Higher toughness than carbide; suitable where chipping resistance and longer reach are priorities. |
S6STA / S6DTH / S6DTP |
|
G2 - Carbide |
Higher cutting speed and wear resistance; requires a rigid, stable setup with controlled runout. |
G2STA / G2DTH / G2DTP |
Key Facts at a Glance
|
Item |
Specification |
|
Insert diameter range |
Ø9.5–114.48 mm |
|
Insert thickness range |
2.38–11.11 mm, according to body group |
|
Standard point angles |
132° or 144°, according to diameter group |
|
Chipbreaker codes |
ST - general; DT - strong chipbreaker |
|
Coolant supply |
Through the compatible drill body; confirm the connection and delivery for the selected setup |
Technical Specifications
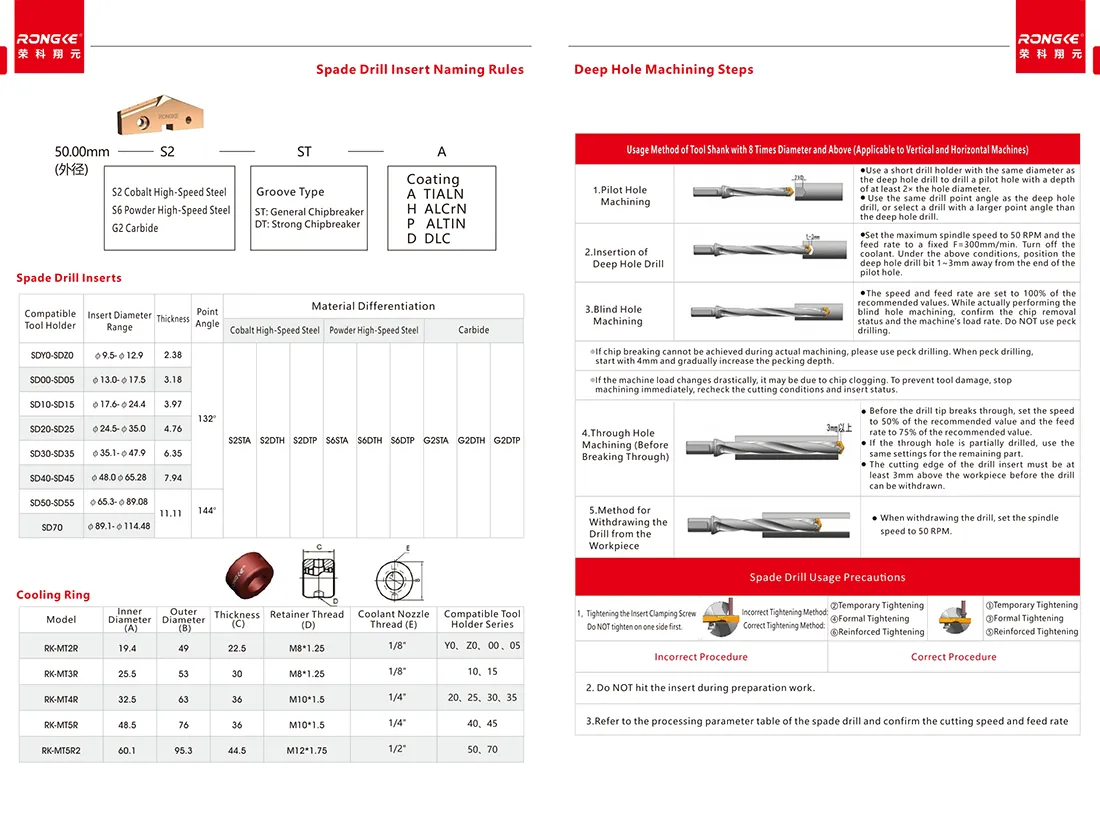
All diameter and thickness values are in mm. Select the Replaceable spade drill inserts code within the corresponding group.
|
Compatible body group |
Insert diameter range |
Thickness |
Point angle |
|
SDY0–SDZ0 |
9.5–12.9 |
2.38 |
132° |
|
SD00–SD05 |
13.0–17.5 |
3.18 |
132° |
|
SD10–SD15 |
17.6–24.4 |
3.97 |
132° |
|
SD20–SD25 |
24.5–35.0 |
4.76 |
132° |
|
SD30–SD35 |
35.1–47.9 |
6.35 |
132° |
|
SD40–SD45 |
48.0–65.28 |
7.94 |
132° |
|
SD50–SD55 |
65.3–89.08 |
11.11 |
144° |
|
SD70 |
89.1–114.48 |
11.11 |
144° |
Insert Naming Rules
Example: 50.00 mm S2STA = Ø50.00 mm, S2 cobalt high-speed steel, ST general chipbreaker and A TiAlN coating.
|
Code group |
Meaning |
|
Substrate |
S2 = cobalt high-speed steel; S6 = powder high-speed steel; G2 = carbide |
|
Chipbreaker |
ST = general chipbreaker; DT = strong chipbreaker |
|
Coating |
A = TiAlN; H = AlCrN; P = AlTiN; D = DLC |
Confirm the available substrate, chipbreaker and coating combination for the required diameter.
Four Checks Before Ordering
Body fit. Confirm the exact diameter, body group, insert thickness and point angle.
Substrate. Choose S2 or S6 for toughness, or G2 for a rigid and stable machining setup.
Cutting geometry. Specify the ST or DT chipbreaker and coating code for the workpiece.
Machining conditions. Confirm hole depth, entry surface, coolant supply, alignment and any pilot-hole requirement.
Application Fit
For steel, cast iron and non-ferrous workpieces, subject to insert selection. Matched assemblies can be used on machining centers, CNC lathes, vertical drills and radial drilling machines.
FAQ
Can Replaceable spade drill inserts be reground?
Inserts with normal wear can be considered for factory regrinding after inspection of the edge and remaining geometry.
Is a pilot hole needed for deep drilling?
At 8D and above, plan a pilot hole using a short body of the same cutting diameter. Confirm the pilot depth and entry procedure for the selected assembly.
Are special profiles available?
Radius, flat-bottom and other special insert profiles can be reviewed against a customer drawing; confirm compatibility with the body.
Inspection and Supply Details
Production & inspection. Check diameter, thickness, point angle, cutting edge, locating pin, seat and clamping screws. Confirm the selected variant, stock and lead time with the quotation.
Quotation Checklist
Send exact diameter, S2/S6/G2, chipbreaker and coating codes, body code, workpiece grade and hardness, hole depth, coolant supply and quantity.
Send Inquiry
Contact Info
-
Address
No. 399 Haohai Road, Binhai New Area, Economic Development Zone, Fenghua District, Ningbo City, Zhejiang Province, P.R.China
-
Tel
-
Email
Request a quotation from RONGKE for standard U drills, modular deep hole drills and customized CNC cutting tools. Share your machining requirements, tool dimensions and order quantity for professional product recommendations.
Related Products
News Recommendations