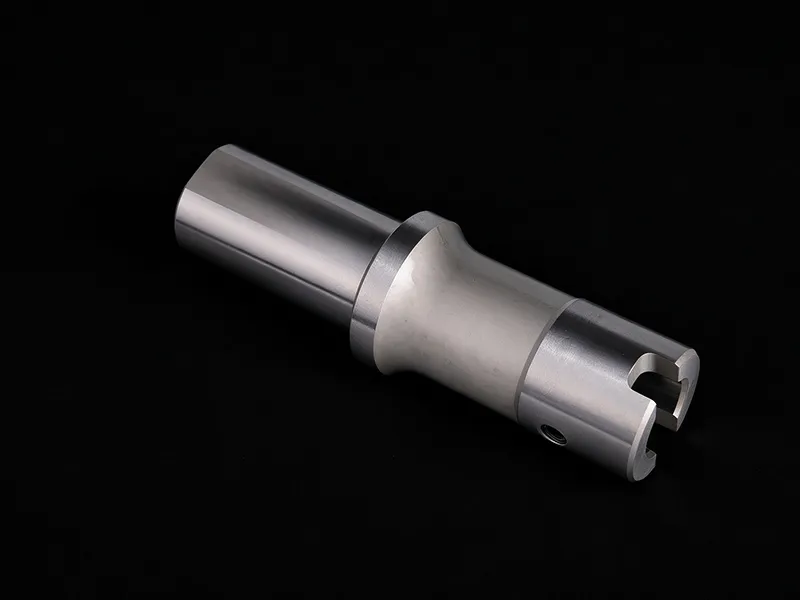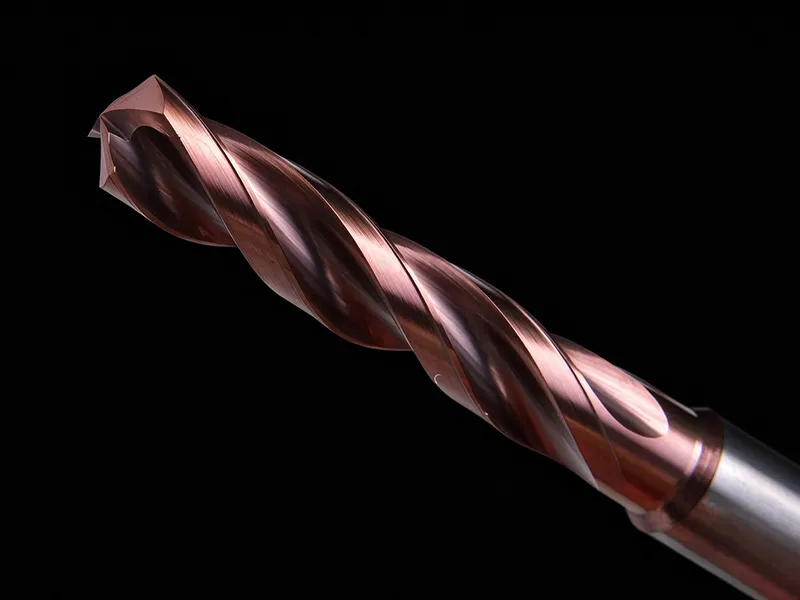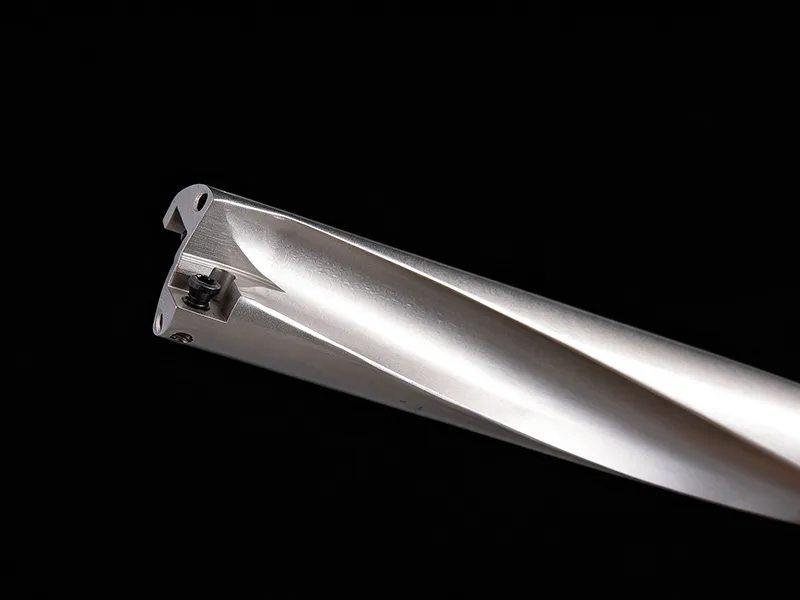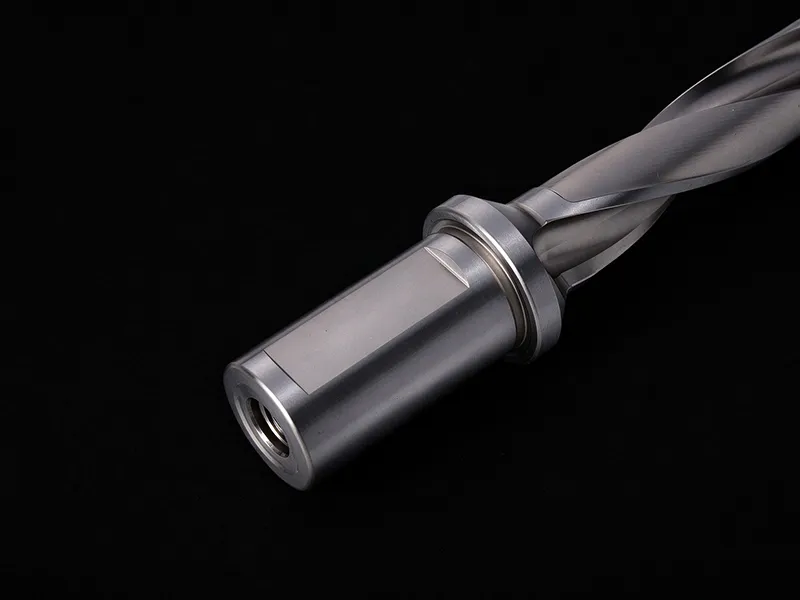
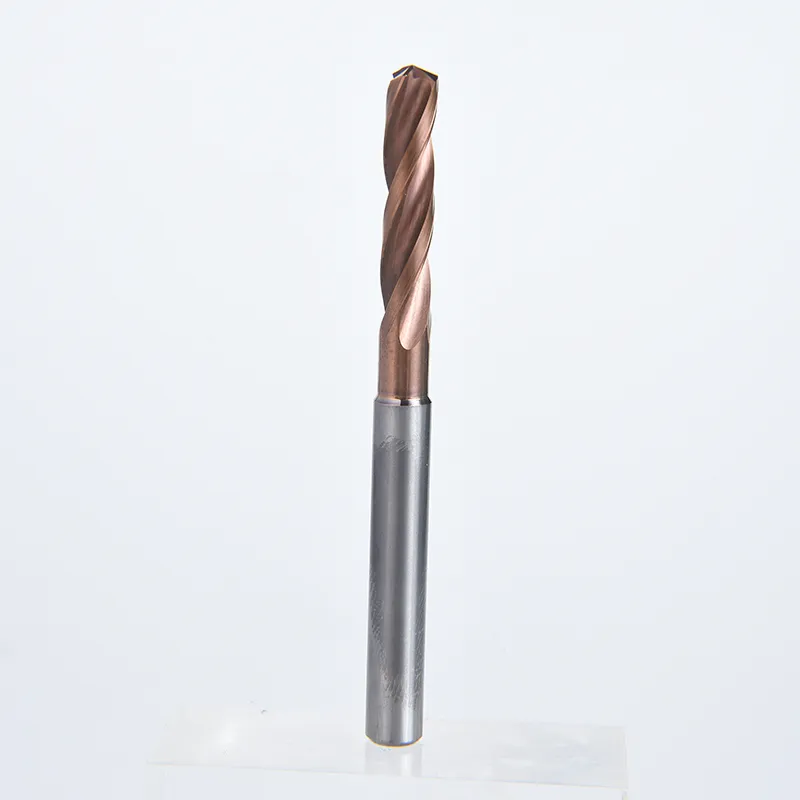
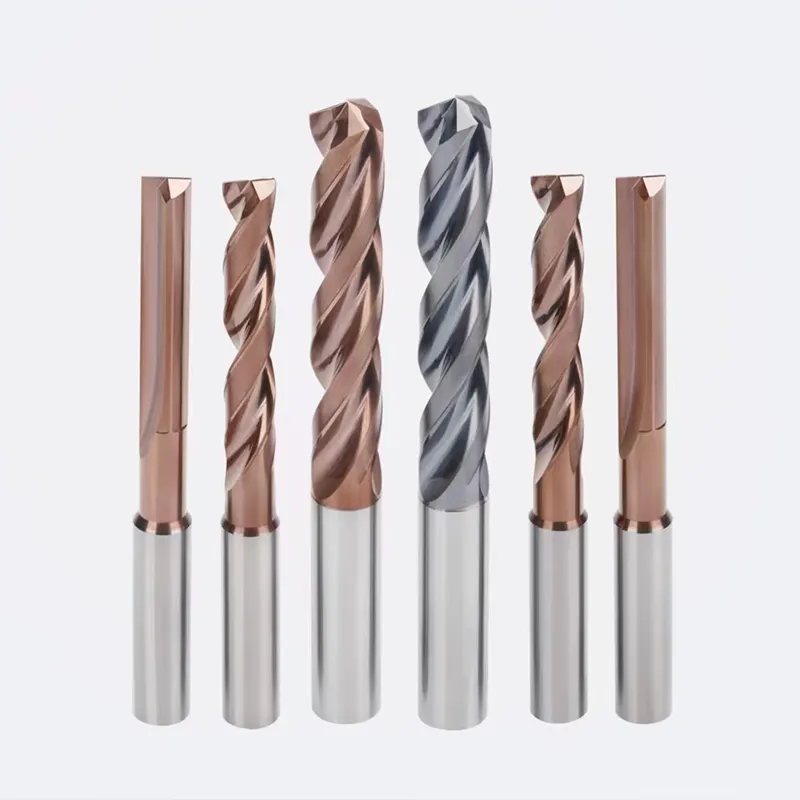
Internal Coolant Solid Carbide Three Flute Micro Drill
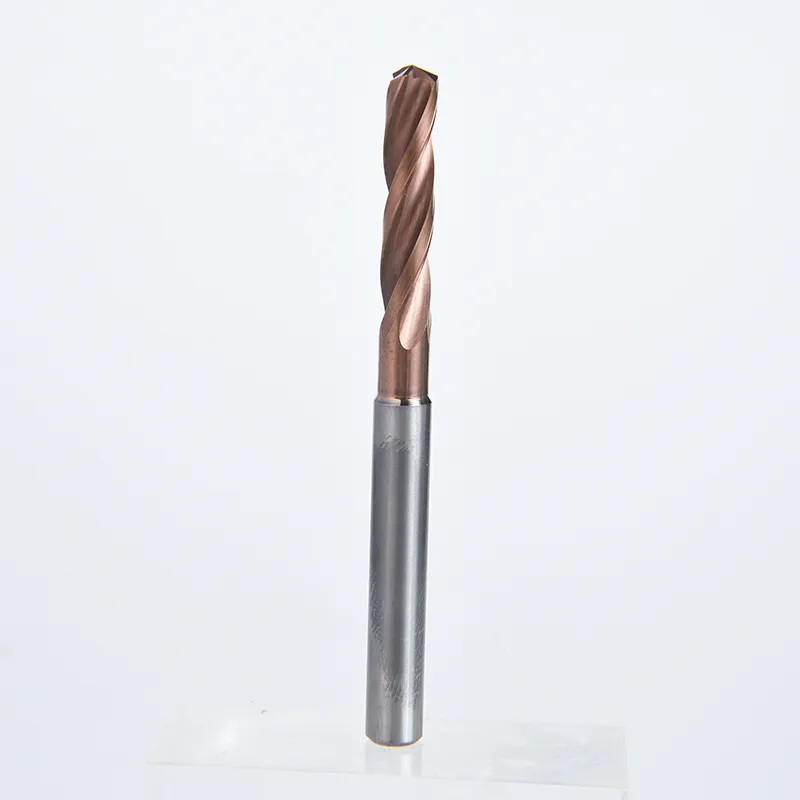
RONGKE supplies the Internal Coolant Solid Carbide Three Flute Micro Drill for CNC drilling where external nozzles have limited access to the cutting zone. Available catalogue depth families are 3D, 5D and 8D, covering Ø5.0–12.0 mm. Contact the China factory with your coolant setup and hole drawing for a quotation.
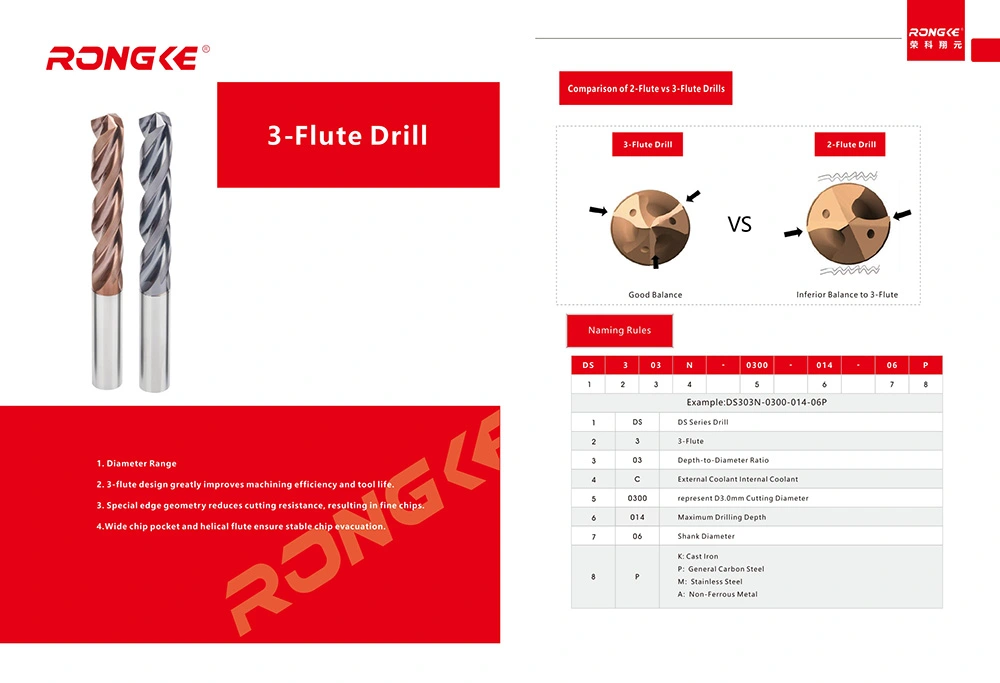
As a China manufacturer and supplier, RONGKE offers the Internal Coolant Solid Carbide Three Flute Micro Drill for buyers who need to match the tool to a through-coolant machine. Its defining feature is the coolant passage: depth remains a separate selection, rather than “internal coolant” being another length series.
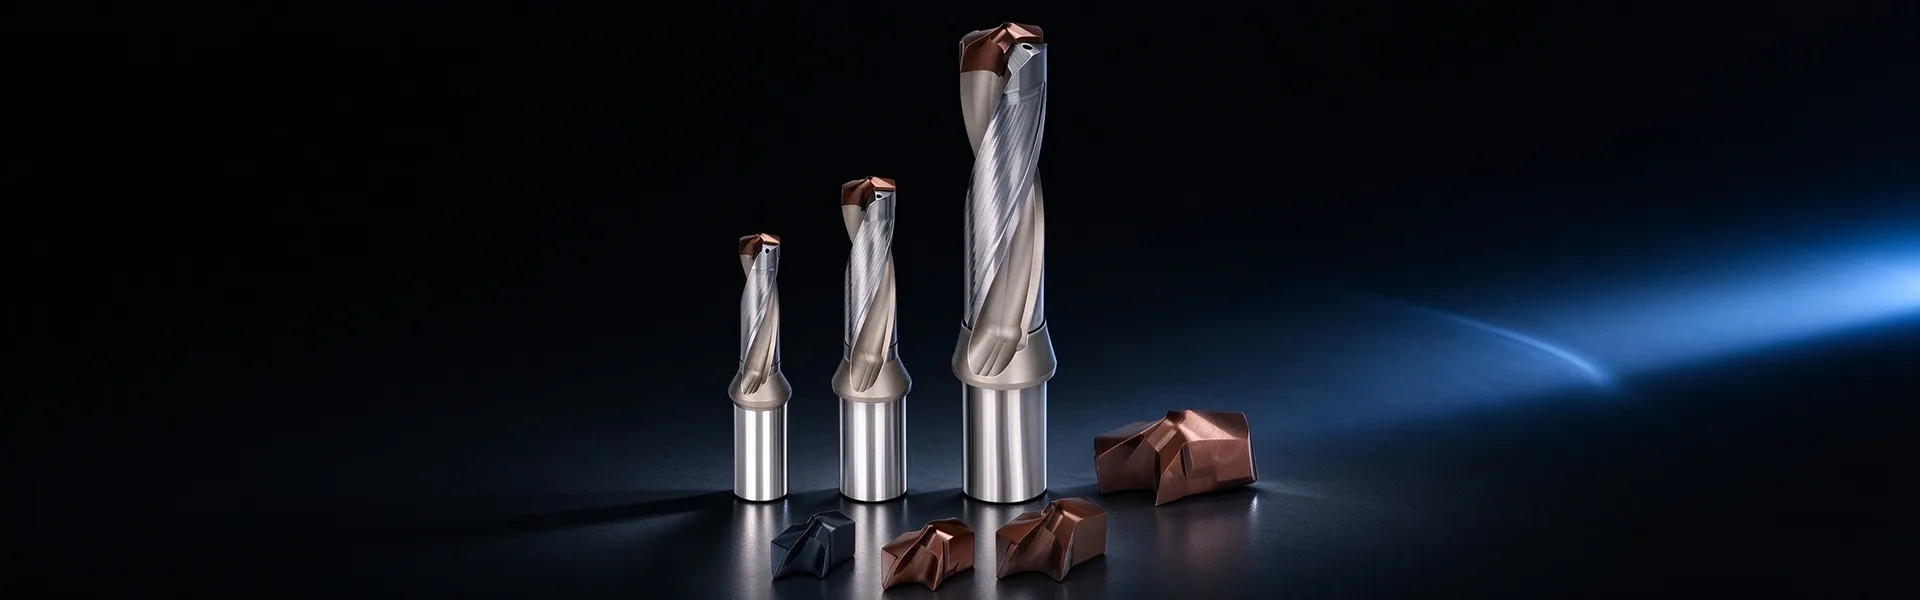
Choose a compact 3D tool for a short feature, or the appropriate 5D or 8D version for greater reach. The holder connection and coolant supply must suit the ordered configuration. Internal delivery does not make an unsuitable material match or unstable setup acceptable.
Working Principle
Coolant enters from the shank end and travels through internal passages toward the cutting edges. Chips leave along the external helical flutes. The fluid reaches an area that an external nozzle may not reach effectively as the hole becomes deeper, supporting cooling and chip evacuation.
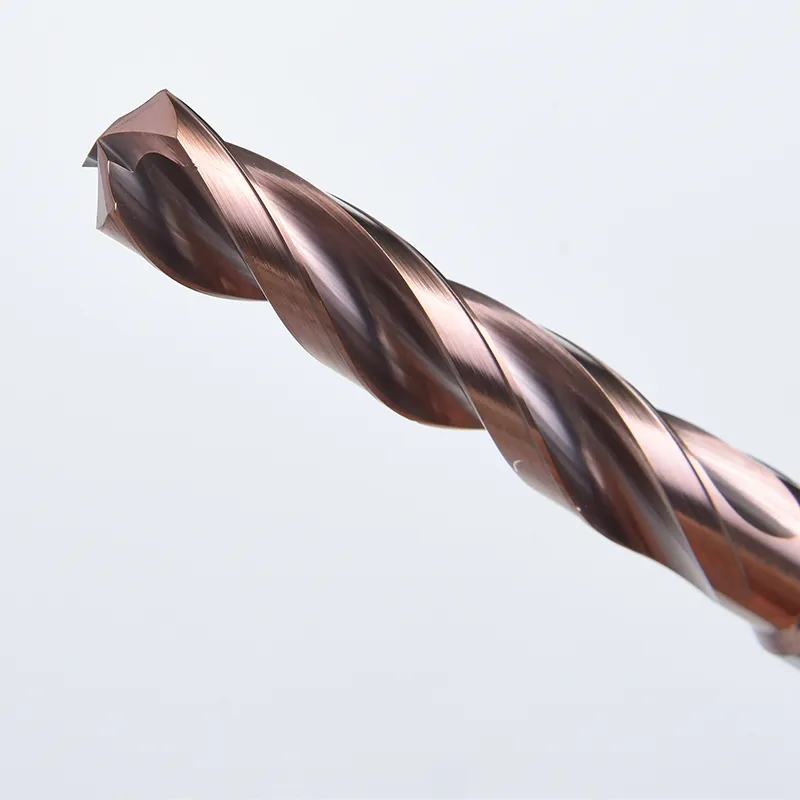
The three integral carbide edges perform the cutting. Correct geometry and feed create chips that the flute and fluid stream can transport; raising coolant pressure alone does not correct every chip-control problem.
Advantages of Internal Delivery
Access near the drill point. The coolant path brings fluid toward the cutting zone inside the hole, rather than relying entirely on flow from the entrance.
Depth chosen independently. Three catalogue length families allow the coolant configuration to be combined with the reach the part actually needs.
A complete drilling system to review. The tool, holder and machine supply can be assessed together before purchase, which is particularly useful when switching from external cooling.
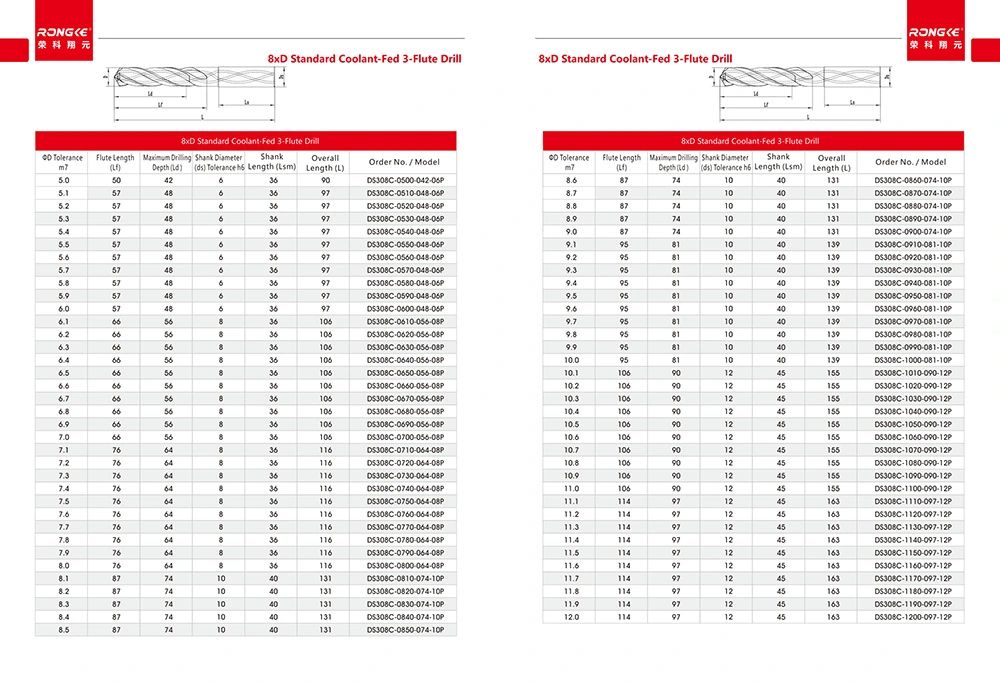
Specifications
|
Item |
Catalogue information |
|
Construction |
Solid carbide; three integral cutting edges; internal coolant passages |
|
Cutting diameter |
Ø5.0–12.0 mm, in 0.1 mm increments |
|
Tool tolerances |
Cutting diameter m7; shank h6 |
|
Shank diameter |
Ø6 / 8 / 10 / 12 mm |
|
Workpiece codes |
P carbon steel; K cast iron; M stainless steel; A non-ferrous metal |
|
Coolant interface |
Shank-fed; holder connection, pressure and flow to be confirmed for the ordered tool |
|
Replaceable cutting parts |
None; this is not a replaceable-head or indexable-insert drill |
|
Depth family |
Max. Ld range |
Flute Lf range |
Overall L range |
|
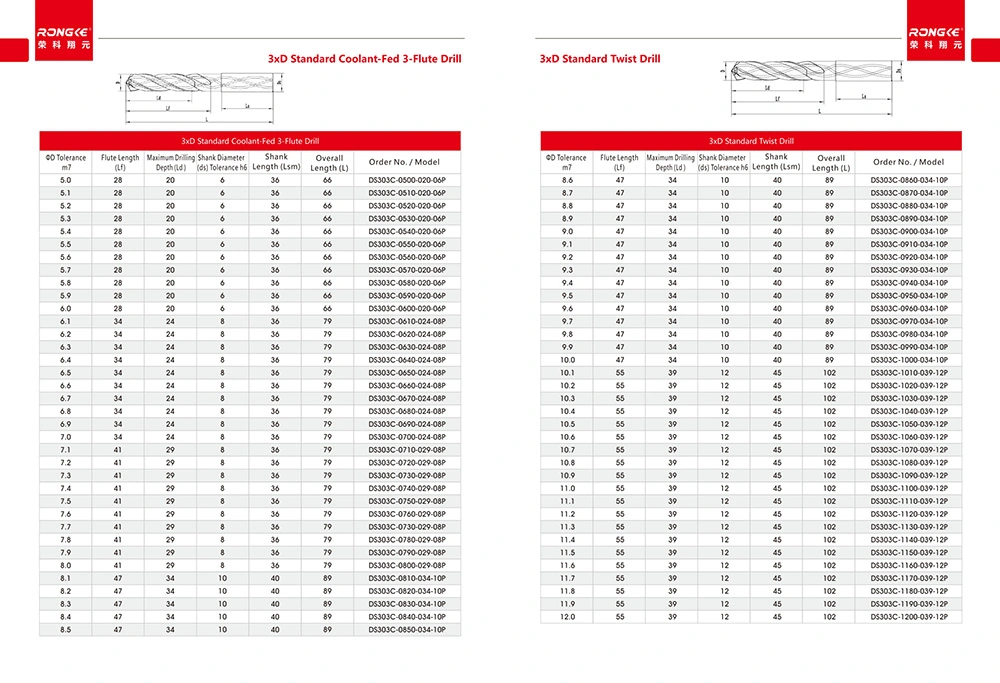
3D / DS303C |
20–39 |
28–55 |
66–102 |
|
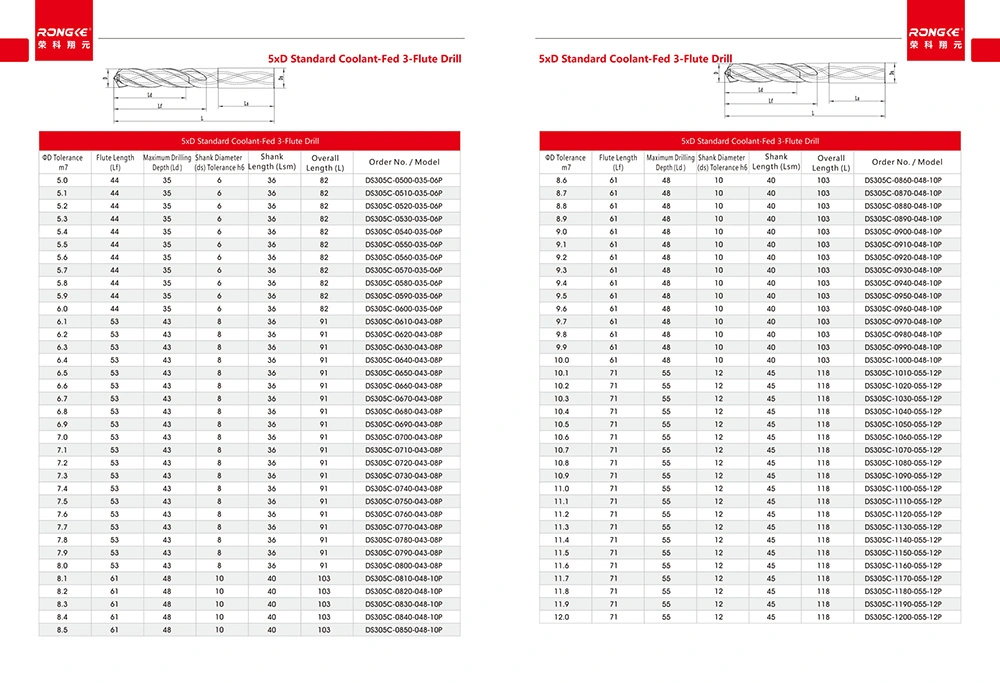
5D / DS305C |
35–55 |
44–71 |
82–118 |
|
8D / DS308C |
42–97 |
50–114 |
90–163 |
Dimensions in mm, grouped across the stated diameter range; values cannot be freely combined. Source: RONGKE MAIN CATALOG, PDF pages 64–67 of 69. Confirm the complete model and internal-coolant configuration on the order.
Application Areas
The Internal Coolant Solid Carbide Three Flute Micro Drill can be considered for blind mounting holes, deeper passages and recessed features in batch-machined components. Its relevance comes from coolant access and chip evacuation, not from an industry label alone. Match the actual material to the P/K/M/A option.
Precautions During Use
Before cutting: confirm coolant reaches the tool outlets and inspect the holder setup. Use the shortest suitable reach and verify run-out.
During the trial: watch for changing cutting noise, spindle load, chips and hole finish. Stop and investigate signs of chip blockage rather than continuing the same cycle.
For blind or interrupted holes: check point clearance, maximum depth and the entry or exit geometry. Do not add a peck cycle or increase feed solely because the tool has three flutes.
General application reference: Sandvik Coromant, Drilling tips — https://www.sandvik.coromant.com/en-us/knowledge/drilling/drilling-tips. These principles do not specify RONGKE pressure or cutting-data limits.
How to Maintain the Drill
Keep the supply path clean. Check coolant filtration and visible outlet flow as part of the setup routine. If flow changes, have the holder and tool passages checked before returning the drill to work.
Inspect wear before it becomes damage. Compare cutting-edge condition and hole results at suitable intervals. Refer a worn tool for professional regrinding assessment before excessive wear develops.
Protect the cutting edges between jobs. Clean the tool with a suitable method and store drills separately so their carbide edges do not strike each other. Keep the model identification with each tool.
Review a reconditioned tool before reuse. Confirm the remaining geometry and usable depth with the reconditioning provider. Recheck coolant delivery and the application setup; do not assume an unlimited number of regrinds.
FAQ
Does internal coolant mean the drill needs a threaded connector?
Not necessarily. The tool is supplied through the shank and compatible holder arrangement. Confirm the actual holder and machine interface; the catalogue pages do not specify a universal threaded connection.
What pressure should I use?
There is no catalogue pressure value that applies to every listed diameter and depth. Provide the machine’s pressure and flow capability, material and hole details for an application review.
Can it run on a machine with external coolant only?
External supply may suit some shallow-hole applications, but it does not reproduce delivery through the internal passages. Ask for a suitable tool and process assessment before using this configuration without through-coolant.
Does this version replace the 3D, 5D and 8D products?
No. Internal coolant describes fluid delivery; 3D, 5D and 8D describe depth families. A tool can belong to a depth family and have internal coolant at the same time.
What if chips start packing in the flutes?
Review chip shape, coolant delivery, cutting-edge condition and the selected cutting data. More pressure alone may not solve the cause. Stop the cycle if the cutting behaviour becomes abnormal.
Can the tool be reground?
Reconditioning depends on wear and remaining tool geometry. Have a qualified provider assess the drill, including the coolant outlets, and confirm usable dimensions before putting it back into production.
What is needed for a price and suitability check?
For the Internal Coolant Solid Carbide Three Flute Micro Drill, provide diameter, effective depth, hole type, material, tolerance and quantity, together with holder details and coolant capability. Include a drawing if the feature has cross holes or an uneven entry.
Related Category
Send Inquiry
Contact Info
-
Address
No. 399 Haohai Road, Binhai New Area, Economic Development Zone, Fenghua District, Ningbo City, Zhejiang Province, P.R.China
-
Tel
-
Email
Request a quotation from RONGKE for standard U drills, modular deep hole drills and customized CNC cutting tools. Share your machining requirements, tool dimensions and order quantity for professional product recommendations.
News Recommendations